Three Peaks Challenge for Tiny Tickers

Three Peaks

Three Peaks Challenge for Tiny Tickers

Date: 14th July 2022

On the 9th July at 6:45am, our Dan Milton and his Wife Jemma started their 1st climb up the Ben Nevis as part of the 3 Peaks Challenge. Ultimately, was a tough climb and they met many new faces who joined them on their climb. They summited at 10:00am before descending and jumping on what would be their new lounge & bed – the hot minibus with 12 other people…

The next stop was Scafell Pike, setting off at 20:15 they were under strict orders to climb quickly and be back down by midnight. The climb took place with the sun setting over the neighbouring mountains, and they hit the summit at approximately 22:10. The pace was tough and not all of them made it. The decent involved walking in the dark with their headtorches on to ensure they got down – they arrived at 00:06 for a quick refresh and then on to Snowdon.

They arrived for a quick breakfast and briefing, instructing the group that all of the group will summit Snowdon. They set off at 06:10 and climbed confidently until they summited at 09:05, the Pyg track was the accent and with the morning sun rising in the East made the climb that much tougher as there was little to no breeze. The decent was down the Llanberis Path, which essentially was the end of their journey. Upon the arrival in the village at 12:15 a celebratory ice cold lager went down a treat.

The walk was in support of the charity, Tiny Tickers, in memory of their son Noel who sadly passed away at 8 weeks old, who would now be 12, and this week marks 12 years of him suddenly passing away.

Dan and Jem would like to thank everyone at Air Technology Systems & ATS Plastics for their support and donation. They would also like to thank ATS for making a big donation which kick-started the fundraising to allow them both to undertake the challenge fully sponsored, and also meant the Tiny Tickers Charity received more money. To date they have raised £2,221.00.

For anybody looking to partake in this challenge, and wants to know how much work needs to be put in:

• 15hr 13mins walking
• 41.72km
• 2,919m elevation
• 5,341 Calories burnt
• 21min /km average pace
• 10 litres water
• Lots and lots of sweets, snack, nuts, fruit, and protein bars
• 22hrs in the fun bus traveling from and to Chester Train Station.
A huge congratulations to Dan & Jem in completing this extremely brave challenge, for the best possible cause. 🤍

IPS Pharma – Warehouse & Mezzanine Cooling

IPS Pharma – Warehouse & Mezzanine Cooling

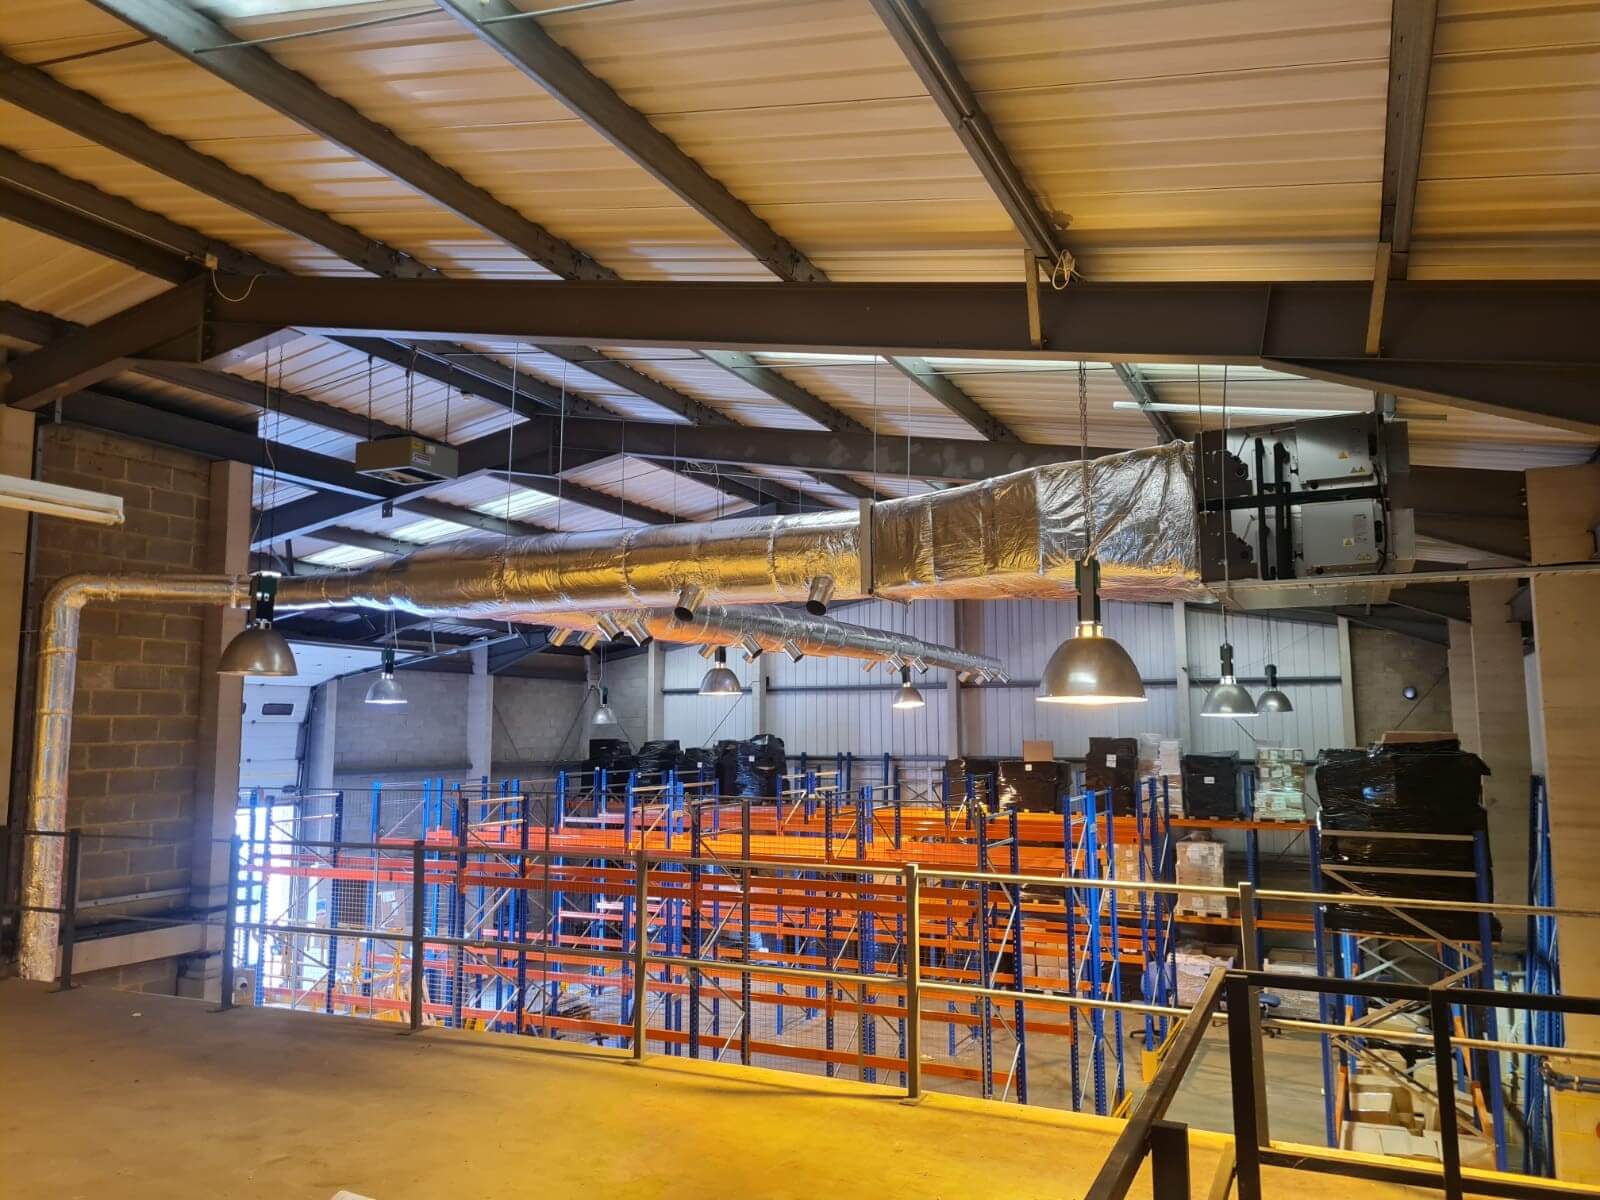
A Heating & Cooling system to meet stringent MHRA guidelines for storage of pharmaceuticals.

Client – IPS Pharma

IPS Pharma are one of the leading manufacturers of Unlicensed Medicines in the UK with over 20,000 formulations available to Primary and Secondary Care.

Project Scope & Objectives

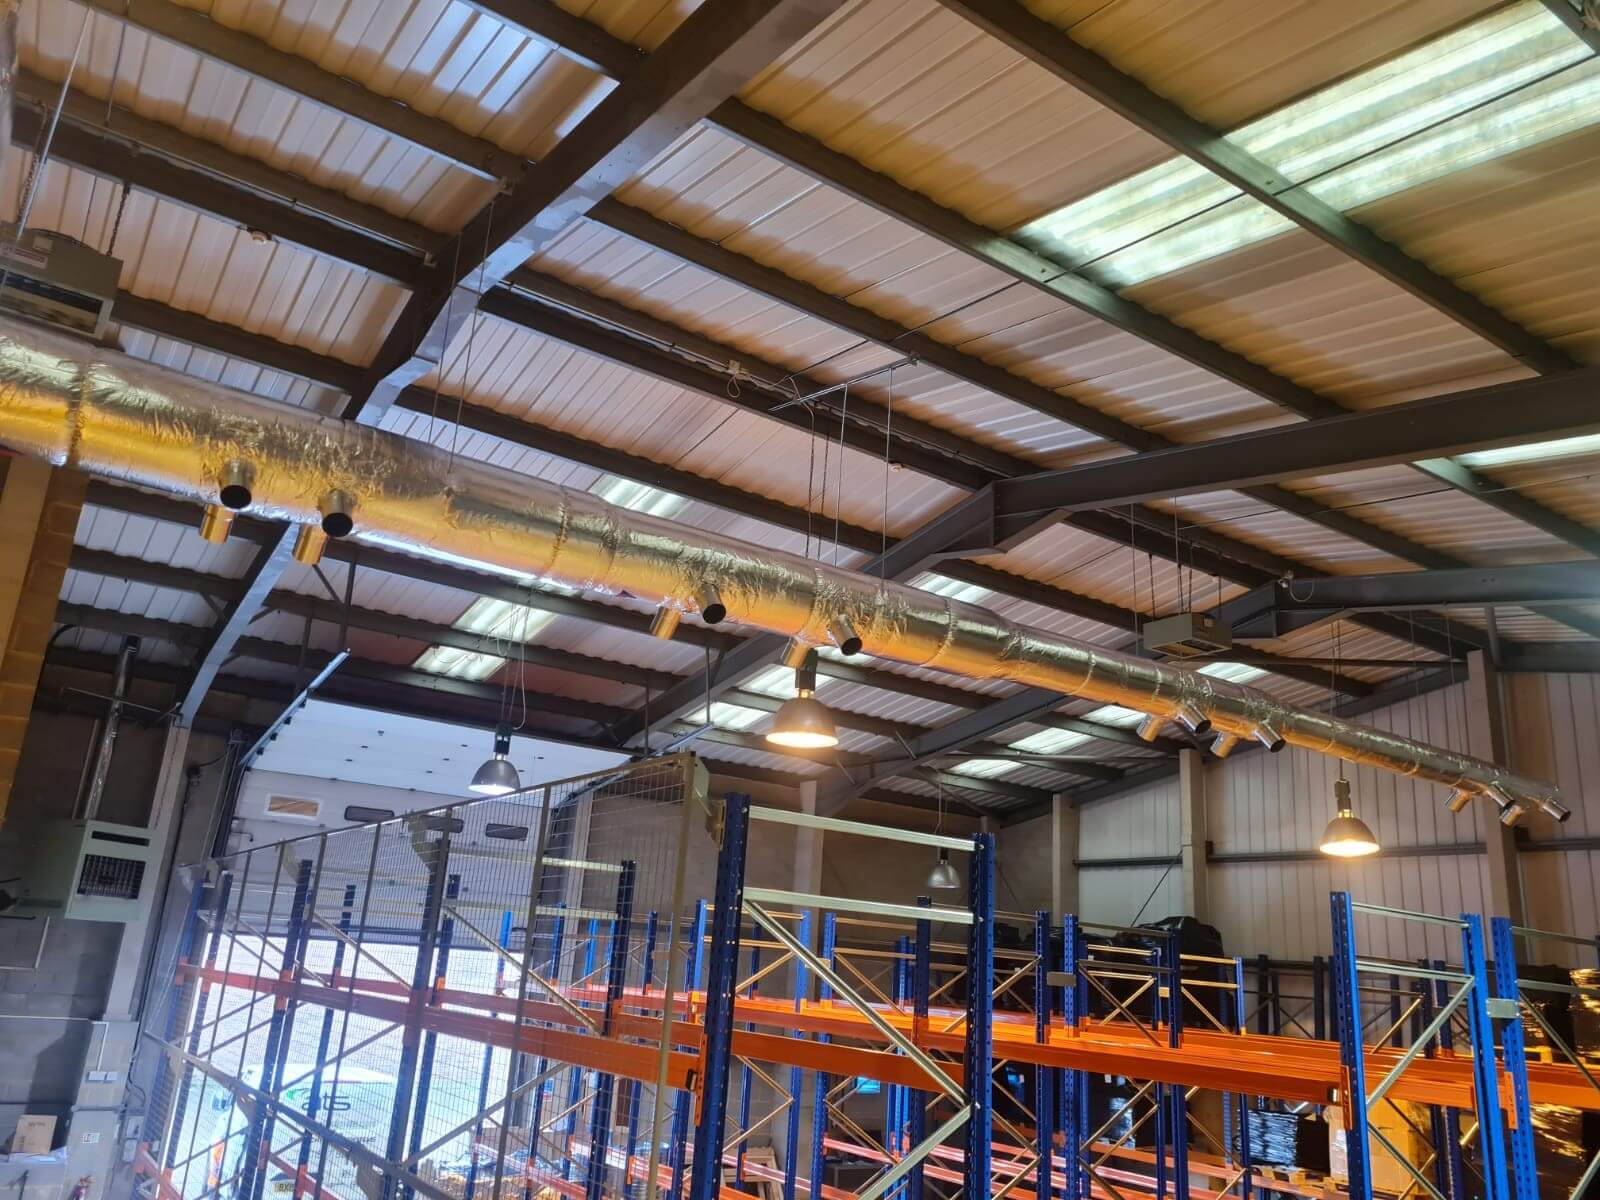
IPS Pharma approached Air Technology Systems to design, supply and install a specialist HVAC (Heating, Ventilation & Air Conditioning) system to a new pharmaceutical storage warehouse. It was crucial that the system maintained a temperature of 15°C – 25°C to meet the current MHRA guidelines, and their stringent product specifications.

Challenges

Air Technology Systems had a few challenges to consider and overcome with this project, from changes in scope of works, to design challenges, all whilst working to a difficult programme.

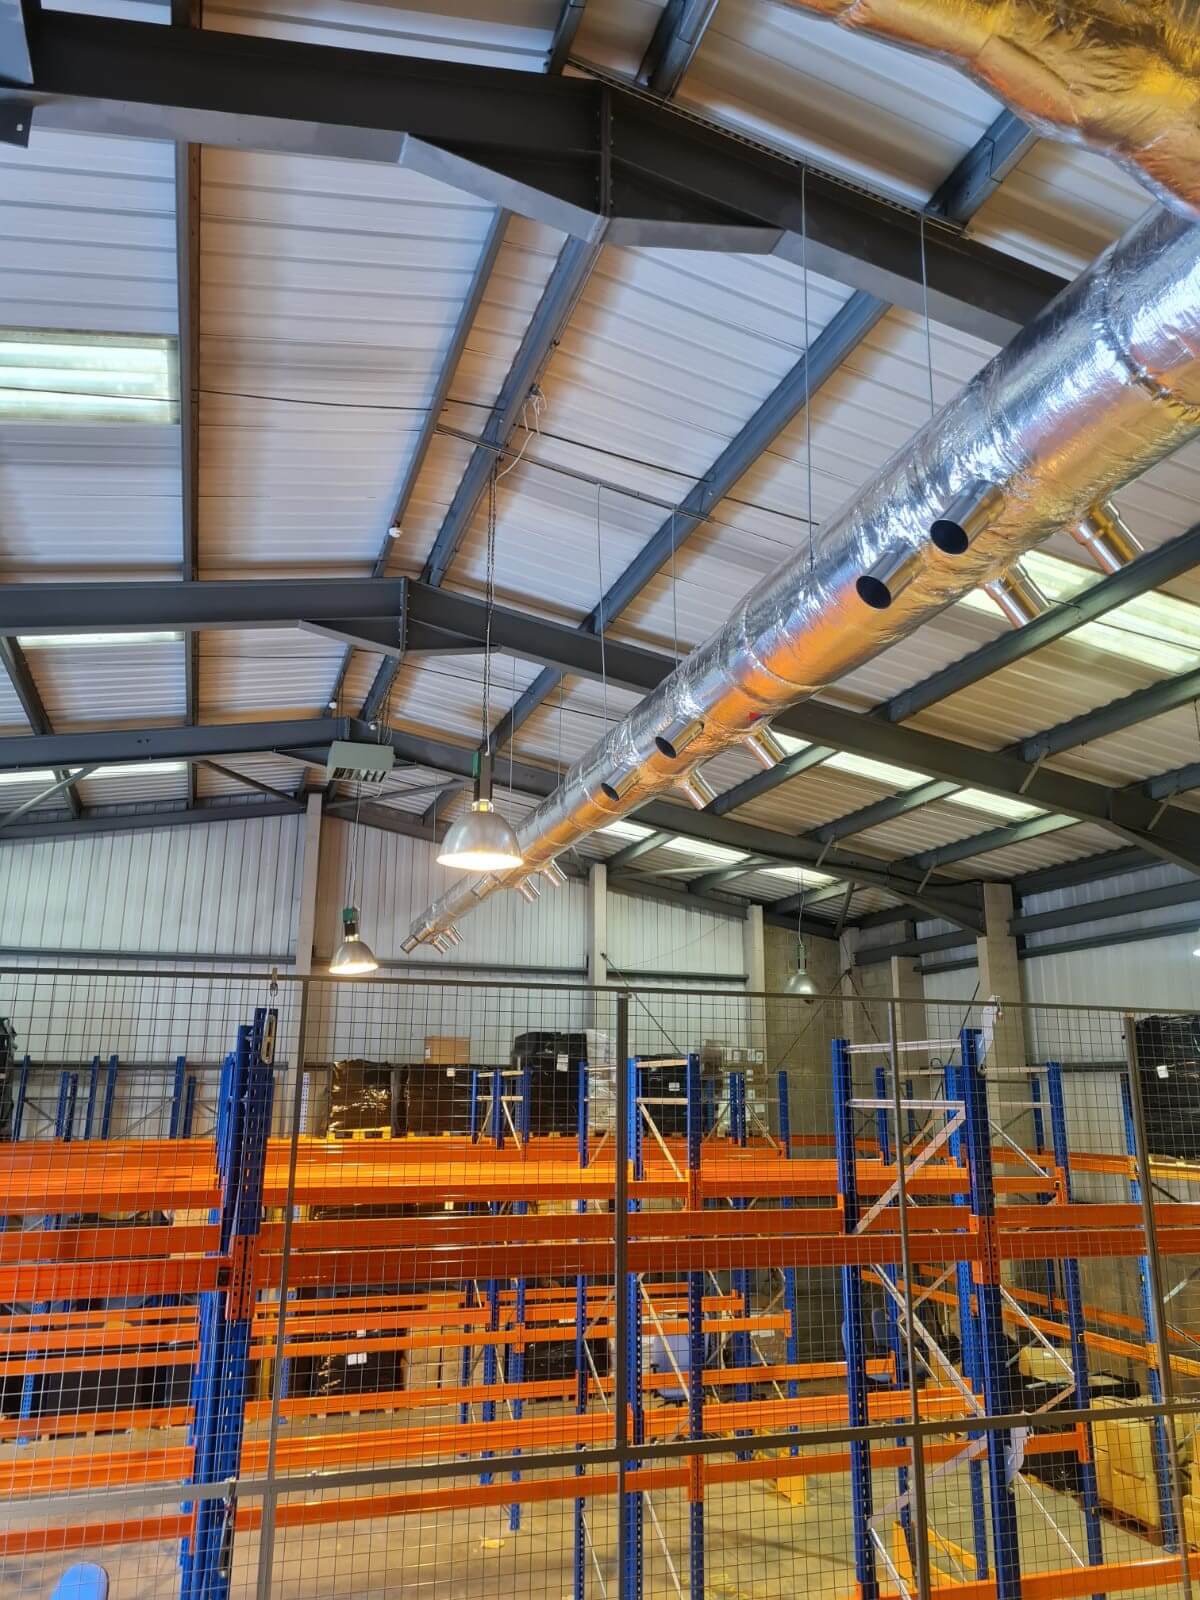
The client asked us to incorporate treating the space underneath the mezzanine area, which wasn’t included in the initial project specification.

The main issue that this presented to our design team was to make sure there was enough airflow and heating / cooling capacity within the proposed system to cover the extra space.

We were also required to make sure there was enough pressure within the system to serve the additional ductwork required to treat the area. All of this needed to be factored in whilst still making sure the costs were in-line with the original budget.

Our client had limited gas on site, so we had to design an all-electric solution with the limited spare electrical capacity available.

Solution

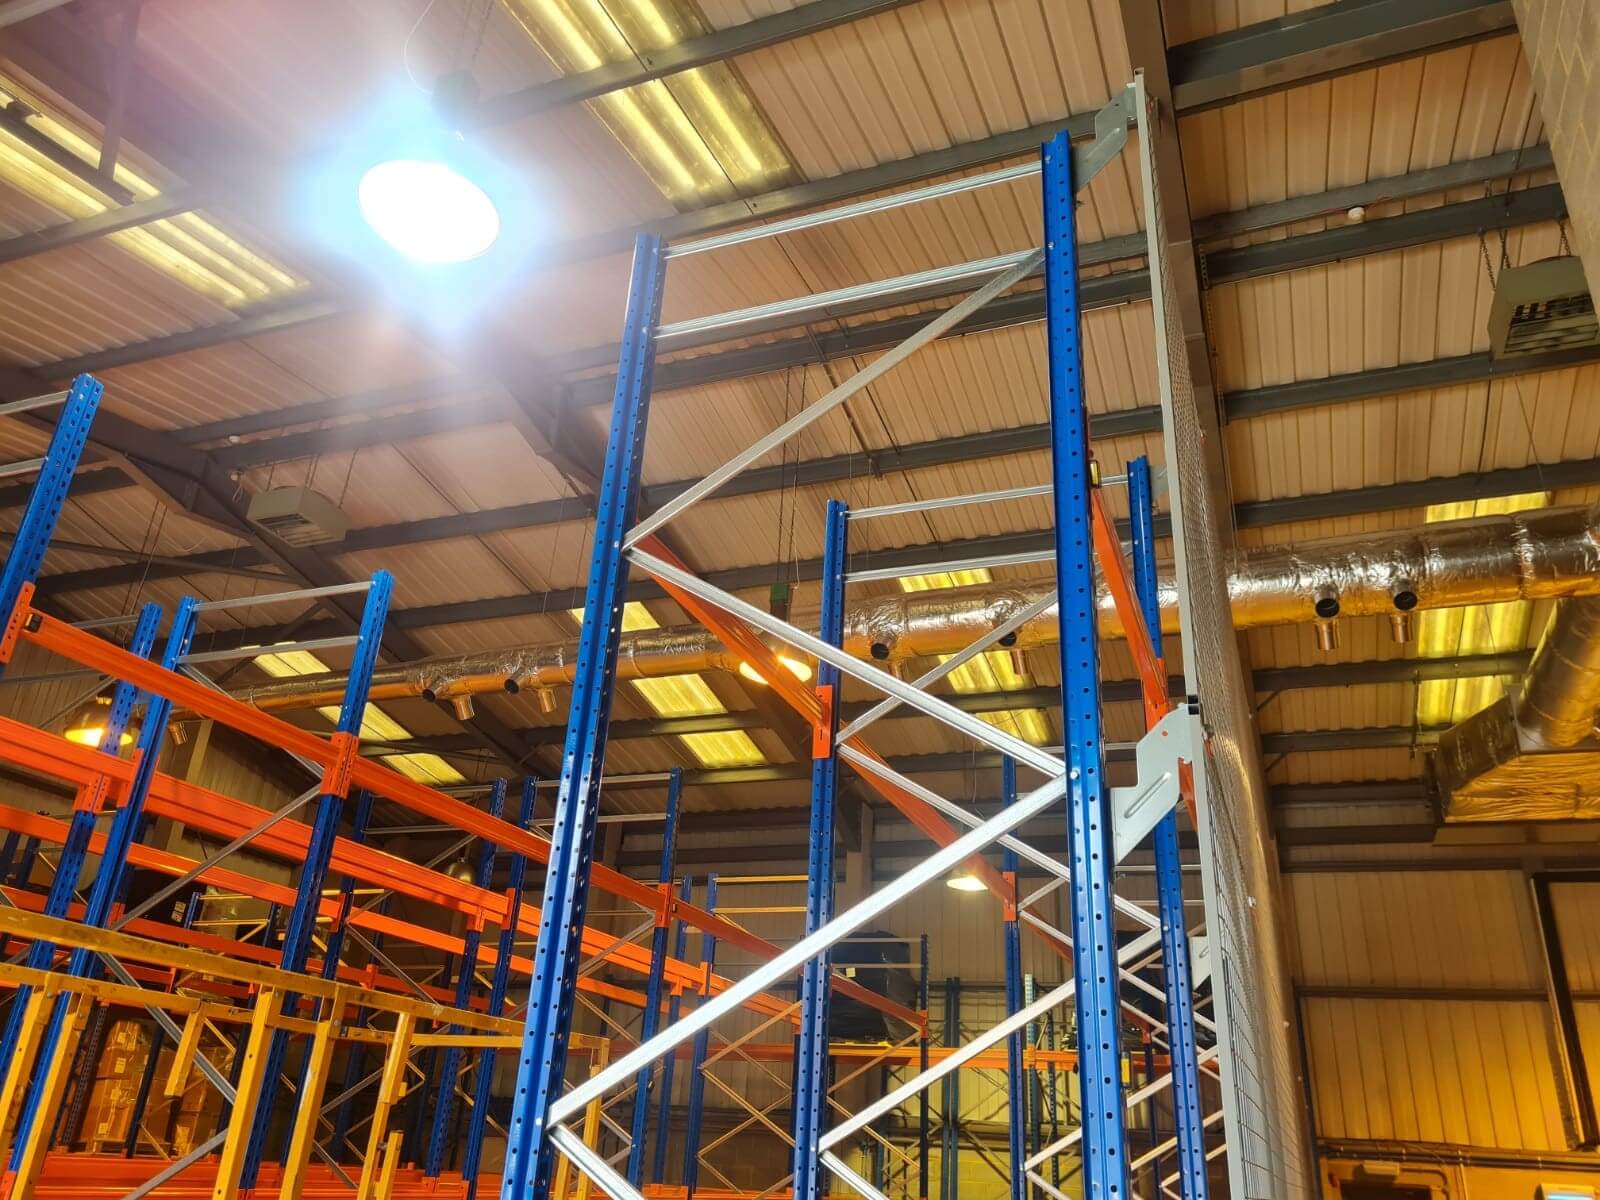
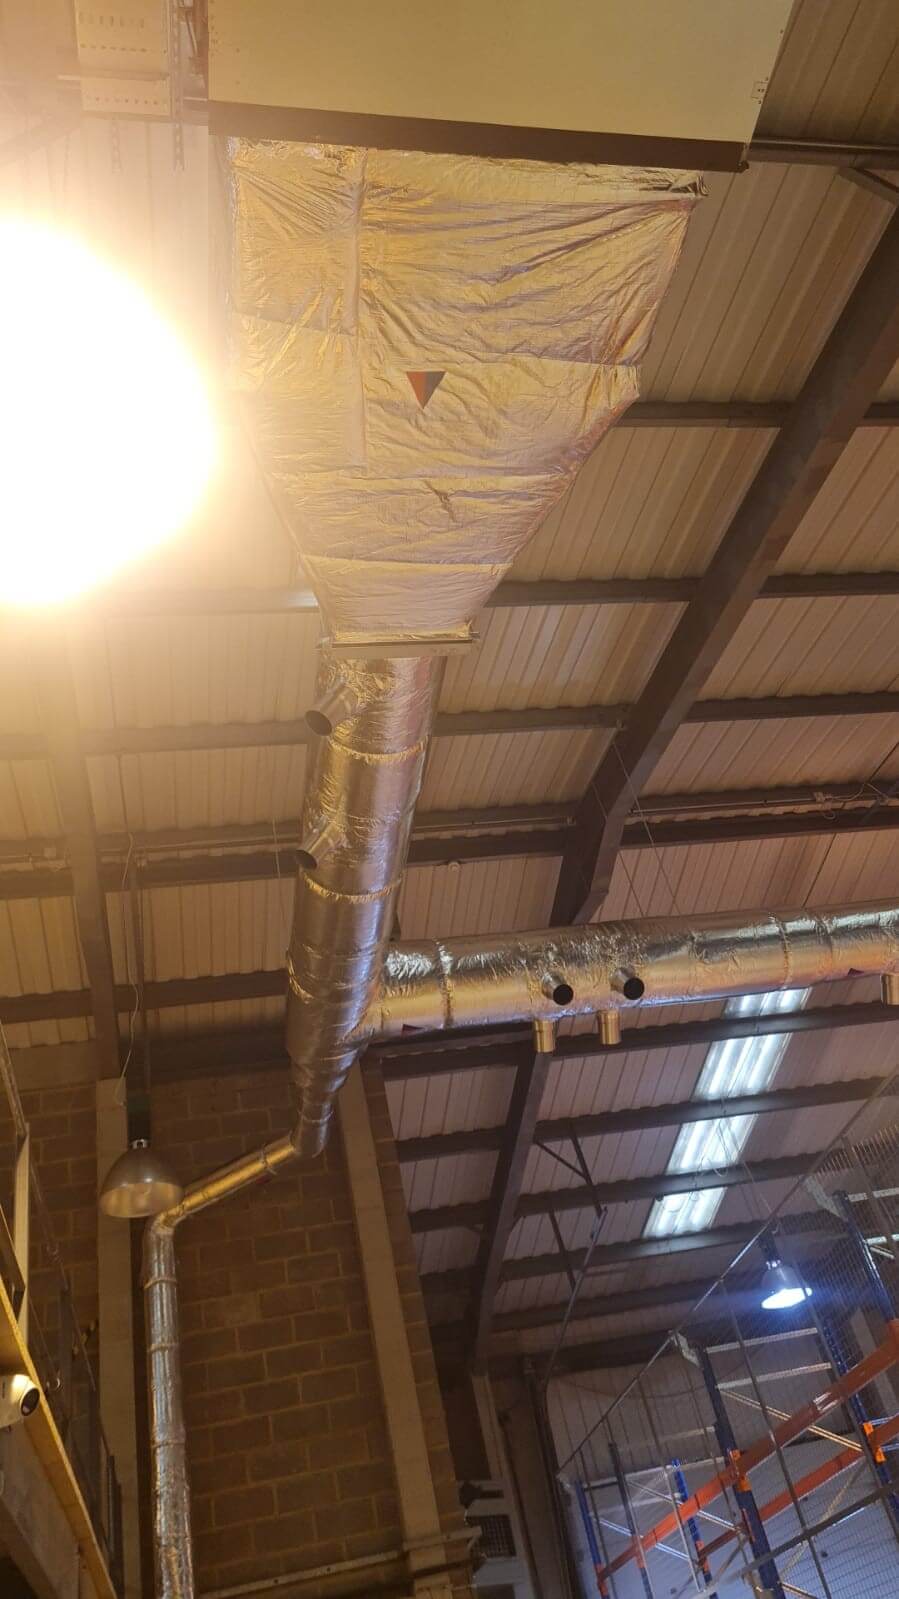
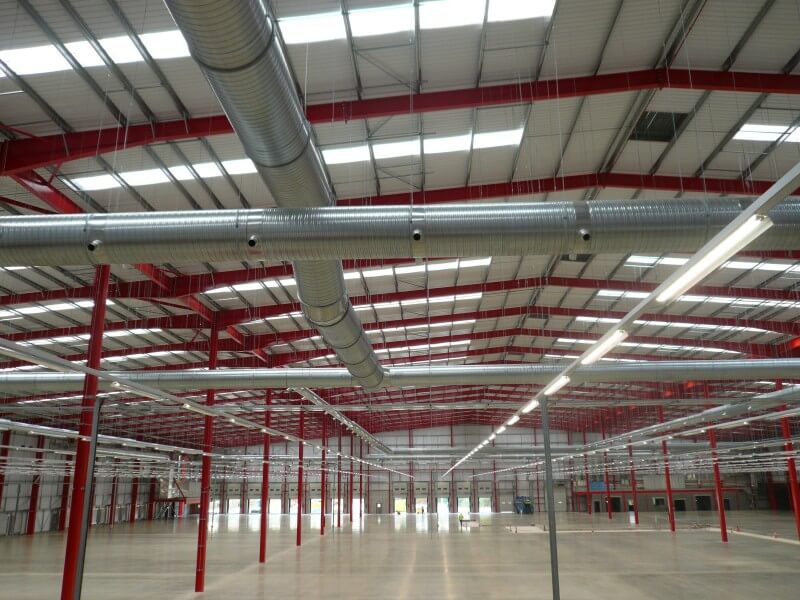
Due to the layout of the warehouse and having to treat underneath the mezzanine, Air Technology Systems came up with an innovative solution to achieve an even air temperature throughout. We utilised air source heat pumps and galvanized ductwork with jet nozzles.

Benefits of us designing and installing an all-electric solution, over a gas-powered system include:

  • More energy efficient
  • Less maintenance
  • Reduce Carbon Emissions
  • Can provide both heating and cooling from one centralised system
  • Lower running costs
Result

Not only is this solution carbon efficient as it is an all-electric solution, but the system also has low running costs and quick installation times, meaning the tight installation deadline was met and within budget.

IPS Pharma now have the peace of mind knowing that the warehouse not only stores its pharmaceuticals within the stringent MHRA requirements, but also meets the stringent manufacturer requirements.

Innovative Ventilation at Purton WTW

Innovative Ventilation at Purton

Innovative Ventilation at Purton WTW

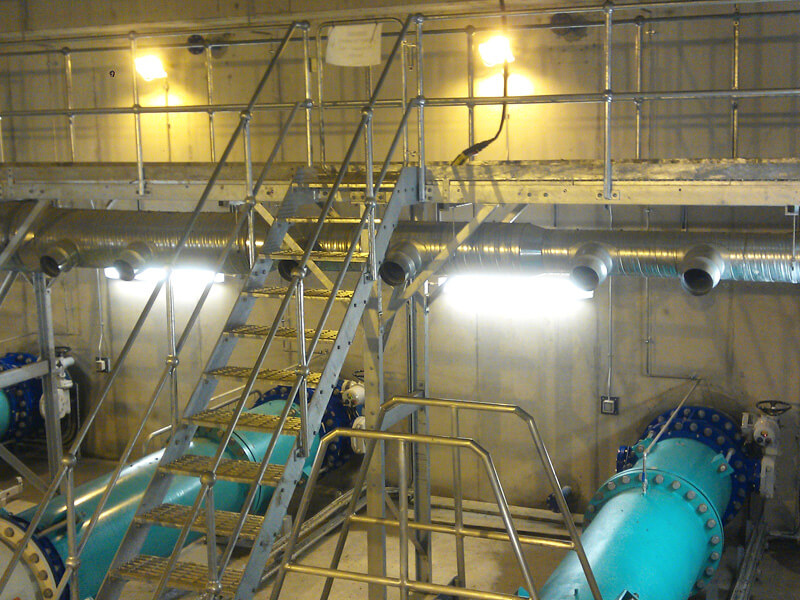
Air Technology Systems Ltd have designed and installed an innovative, energy saving, ventilation and climate control system to serve the control and UV rooms at Purton Water Treatment Works.

Client – Wastewater Organisation

Project Scope & Objectives

The initial specification required the removal of excess heat from the MCC Room and a mercury vapour exhaust system in the UV plant room.

Solution

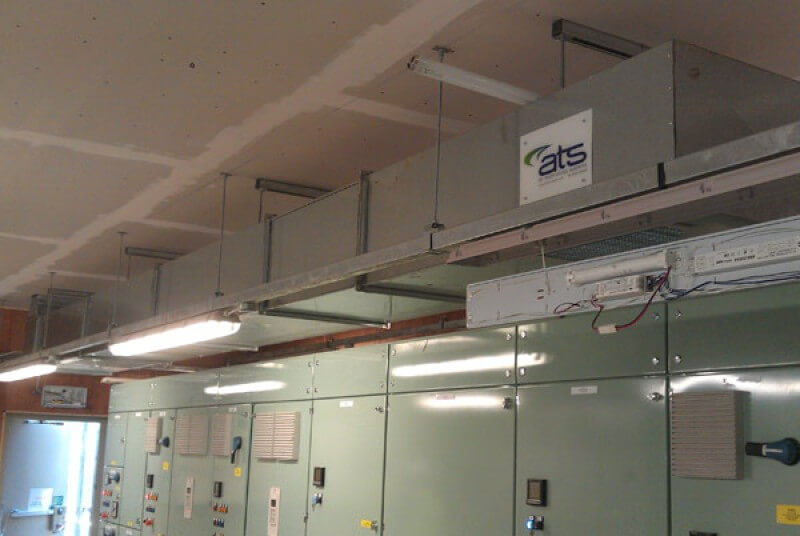
Air is exhausted from the MCC by a range of grilles positioned adjacent to the discharge louvres on the MCC housing and transported via a range of galvanised ductwork. Run and assist fan sets have been included as this room can overheat quickly throughout the year.

The run fan would either send the air to outside (in high summer conditions) or to the UV room (when heat is required), thereby providing free heat at various times. The air will be recirculated to the UV room via our air induction system.

Our Industrial Ventilation System is designed to give a high mixing ratio within the room and ensure that any pockets of gas are quickly diluted, giving an even condition throughout the room. The System works in conjunction with the mercury extract system ensuring that the ‘push & pull’ effect significantly increases the ventilation efficiency. This also reduces the propensity for condensation within the room.

Fresh air is naturally drawn into the MCC via two wall mounted louvres, with open/close dampers, however in hot months the temperature of the UV room will be cooler than the outside air temperature, so we designed the system to recirculate cooler air from the main UV room when appropriate.

The main UV room will generally be a lower temperature as it is below ground and has cool water flowing through it. The air from this room will be recirculated when it is at a lower temperature than the outside air. There is a louvre with open/close dampers mounted within the internal wall for the occasions when the air is being transferred from the UV room. We are therefore taking full effect of the free cooling available from this area.

Within the main UV Plant Room, we allowed for louvres to be provided without motorised dampers, to allow natural exhaust ventilation when air from the MCC is being discharged into the UV room. These louvres will also allow air into the area on the odd occasion when the exhaust extract is on and all the air from the MCC is discharged to atmosphere.

An emergency mercury vapour exhaust system is included for the potential occasion when a lamp may be broken in transit within the room or when the lamps are being changed. This discharges to atmosphere.

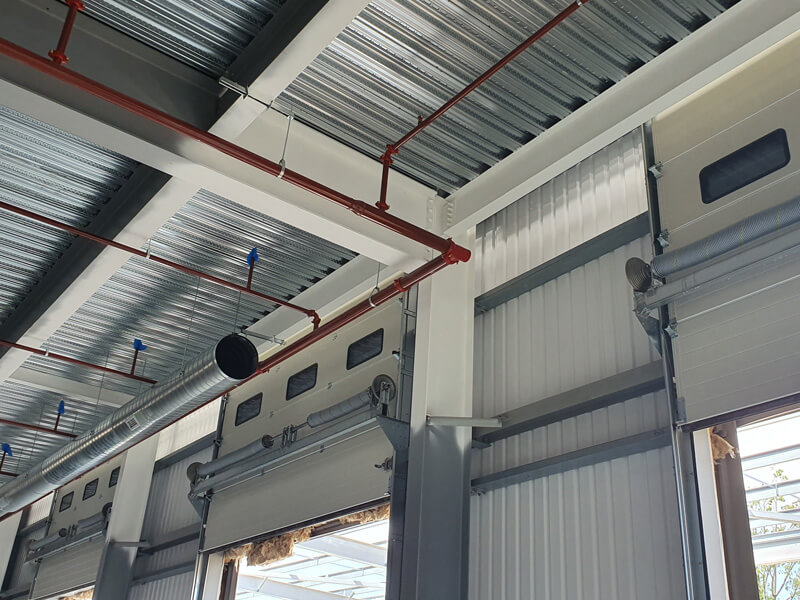
HVAC Solution for a New Aluminium Casting Facility

HVAC solution

HVAC Solution for a New Aluminium Casting Facility

Air Technology System provided a Heating & Ventilation System for one of the world’s premier suppliers of body, chassis, and engineering solutions to the automotive industry.

Client – Magna International

The building services company, Hartle Ltd, engaged ATS on this project for Magna International.

Project Scope & Objectives

Air Technology Systems was asked to provide a heating & ventilation solution for Magna’s purpose-built aluminium casting facility, in Telford, for supplying automotive parts to Jaguar Land Rover.

We were required to design, supply, and install a system to create comfortable and safe working environments across the foundry, offices, and shipping areas, within the project site.

Challenges

There were a number of challenges for this project, not least:

  • The sheer size of area with the main building, a twin span portal frame with lean-to sides, and shipping area occupying 225,000 ft²
  • The vastly different ambient temperatures across the different areas
  • Installing the ducting into the tight space between the crane rail that ran the length of the building and the ceiling height
  • The specified siting of the Air Handling Units (AHUs) on the roof
  • Meeting the specification for 80m³/second of air entering the foundry area

Solution

We designed and installed a displacement ventilation system at low velocity from air supply diffusers, 3m above the finished floor level. To help bring energy costs down, the extract air is taken from the building and re-circulated.

A base fit-out for all service pipework, which included a medium water pressure heating system, vacuum compressed air, and nitrogen and oil lines, ensured machinery and equipment could run smoothly and efficiently.

Result

Our system provided ventilation, a low-pressure water heating system and above ground drainage to remove soil, waste, and water.

We successfully worked with and around the multiple site contractors to deliver all of the project goals. The four AHUs were each delivered to site in three pieces and craned up to the roof.

Our role in this outstanding new facility helped Magna International complete the West Midlands’ largest automotive development, after the Jaguar Land Rover complex, which is also in Telford. The new facility has also created around 300 jobs for Magna International and hundreds more in the supply chain.

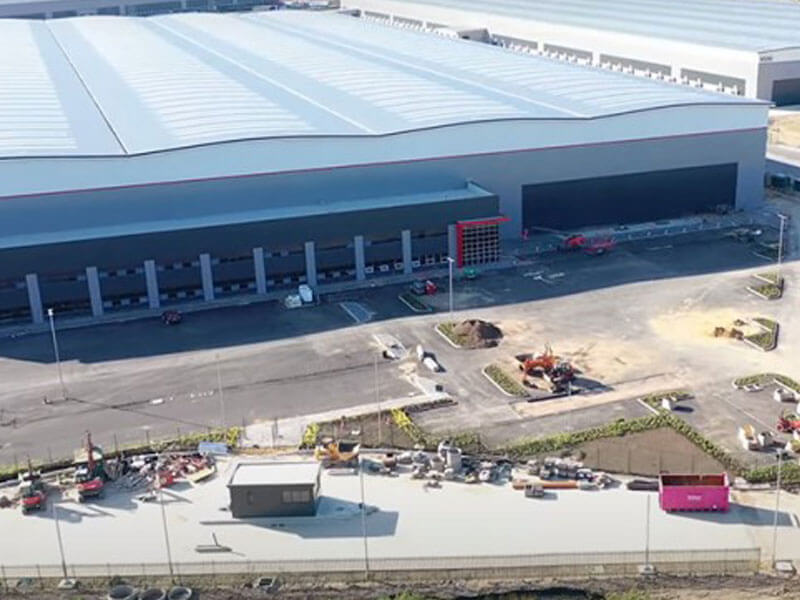
Heating, Cooling & Ventilation System: A new Storage & Distribution Warehouse

M&S warehouse case study

Heating, Cooling & Ventilation System: A new Storage & Distribution Warehouse

Air Technology Systems’ Industrial Heating solutions are highly efficient in solving climate control issues in Warehouse & Distribution Centres.

Client – M&S

Project Scope & Objectives

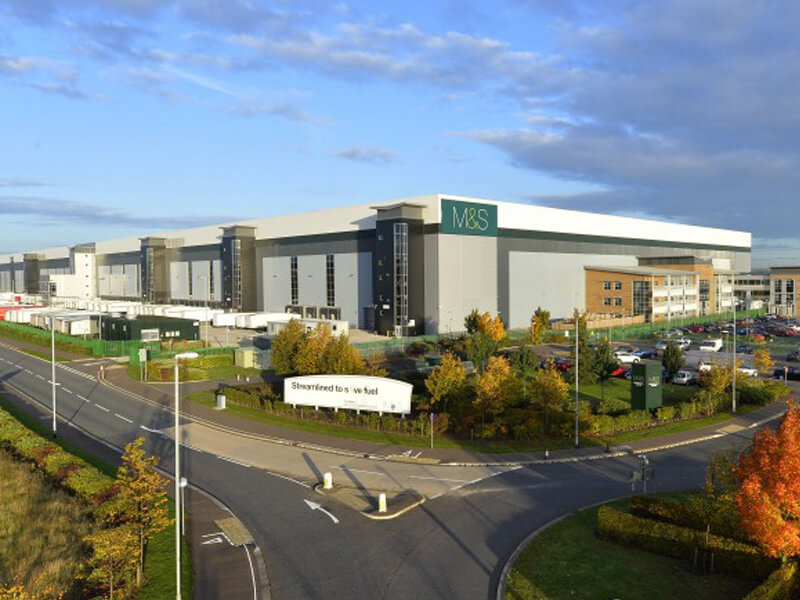
Following the successful design and installation of ten air induction systems in a 1,000,000 ft² warehouse for Marks & Spencer in Bradford, Air Technology Systems was asked to design and install a heating, cooling and ventilation system for the company’s new storage and distribution warehouse, at East Midlands Distribution Centre (EMDC).

The new heating, cooling and ventilation system at EMDC needed to provide an even, temperature-controlled environment for the warehouse, while also meeting M&S’s needs:

  • Stringent environmental requirements
  • Target of 100% ventilation efficiency
  • Requirement for the lowest possible ongoing energy costs

Our distribution centre heating systems are designed to suit your requirements. We offer a free site survey as well as help and guidance with your distribution centre heating requirements. We looked at the logistics of a building, such as opened doors where heat escapes and ceiling height. Distribution centre heating must be kept free of condensation. The intake of cold mainly takes place in loading and unloading areas. Our systems are economic and consider energy saving for low operating costs.

  • Heating zones in the loading and unloading distribution warehouse areas
  • Ensuring warehouse heating requirements in the storage and commissioning area
  • Separate heating of selected areas
  • Energy-efficient heating for the reduction of distribution centre heating operating costs

Challenges

Being a large distribution centre warehouse with a floor area of just under 80,000m² and a ceiling height of 25m, there were several challenges to overcome, including:

  • Infiltration of outside temperatures, through large loading doors
  • Maintaining even temperatures down narrow high-bay racking aisles
  • Potential for overheating in raised mezzanine areas

In addition to the physical challenges of a building of this size and setup, were the considerable environmental and efficiency requirements of this particular blue-chip client.

Solution

To achieve all the project goals required, Air Technology Systems designed a series of systems consisting of:

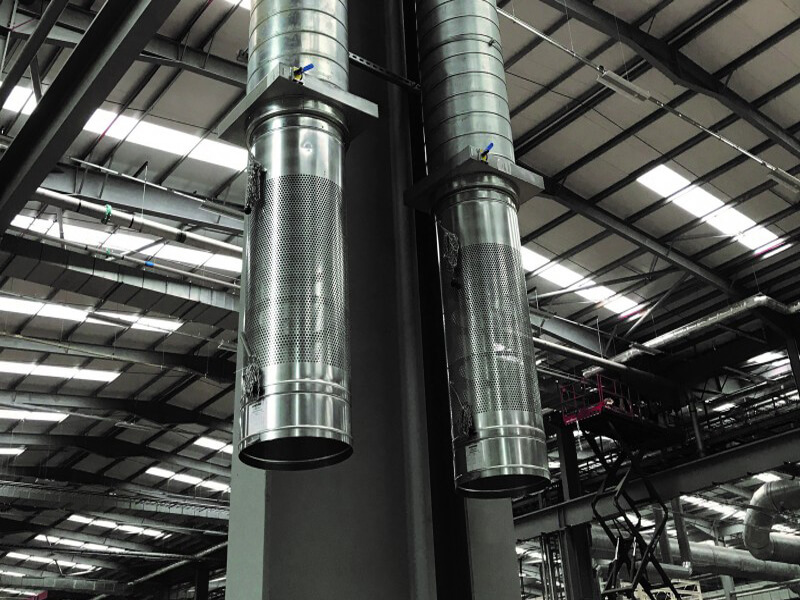
  • Our proprietary air induction nozzle system technology and ducting
  • Externally located Air Handling Units (AHUs), from the Government’s
  • Carbon Trust energy technology list
  • A 4,500m² solar wall

Result

  • The systems’ low volume nozzles enable continuous air recycling of excess heat from lighting and MHE gains, reducing the energy and costs required to maintain temperatures
  • Conditioned air is conveyed to desired areas, minimising stratification and eliminating differential temperatures for 100% Distribution Centre ventilation efficiency
  • The controls strategy encompasses a free Distribution Centre cooling mode that enables cooler night time air to reduce the amount of mechanical cooling required at peak times – reducing carbon emissions
  • The AHUs Carbon Trust credentials ensured increased efficiency and reduced energy usage
  • Our integrated Industrial Climate Control Systems and the 4,500m² solar wall will save M&S in excess of 1,300 kWh and 256 tonnes of CO² per year to help achieve the company’s strict environmental criteria

Europa Worldwide Praise Corby Project

Corby

Europa Worldwide Praise Corby Project

ATS were tasked with providing Industrial Cooling to 3no. mezzanine levels for a project based in Corby.

Client – Europa Worldwide; a global wine stockist.

Project Scope & Objectives

The brief was to maintain the mezzanine levels below 28°C with a flexible approach to controlling the different floors with a Siemens operated system. To achieve this ATS installed 6 no. axial in line duct mounted fans complete with attenuation and 6 No. DX Cooling coils to achieve the required room temperatures with 14 No. external condensing units to supply the coils. 4 units per coil on the 3rd, 2 units per coil for 2nd and 1 unit per coil for the 1st floor to meet the required demand.

Challenges

The electrical and controls for the system were somewhat different to our usual scope and the Design Team of Abdullah, Craig and Darren worked well to come up with a solution to satisfy the requirements.

Solution

The install began in early April under very strict government COVID 19 guidelines and the site team of David N, Derek and Steve P ensured that all procedures and RAMs were adhered to by both internal and subcontractor labour.

With several suppliers ceasing manufacture during this period, it is testament to the entire Team that the job was completed within the required program dates and with Air Technology Systems receiving positive feedback and praise for our performance during the project from the client.

Corby Project Europa

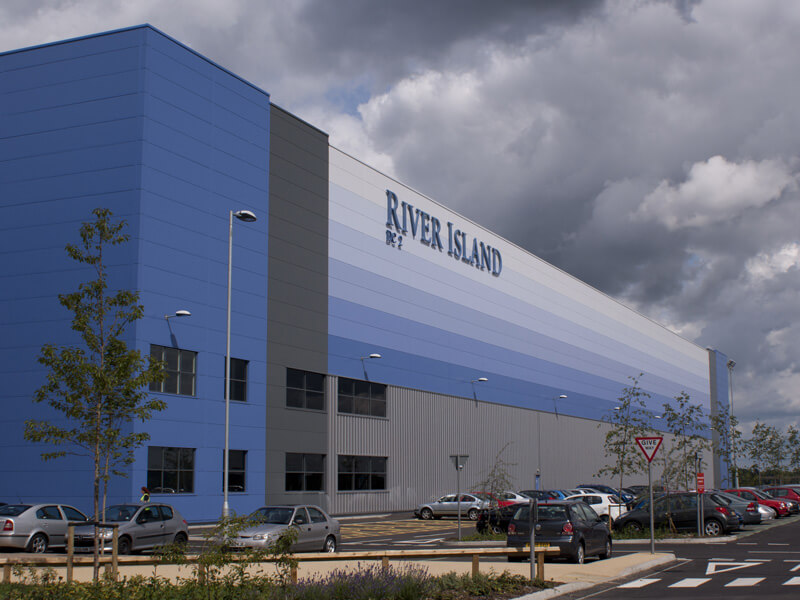
River Island Mezzanine Solution

River Island case study

Climate Control Solutions for Mezzanine Areas at River Island

ATS can offer the most cost effective and low carbon solution for climate control within warehouses fitted with mezzanines, either as a dedicated system or as part of the overall warehouse solution.

Client – River Island

Project Scope & Objectives

When River Island decided to relocate its distribution super centre to Milton Keynes, it called upon Air Technology Systems to provide its Heating, Cooling and Ventilation Solution that would meet its sustainability requirements and its specific business needs within a mezzanine area, whilst utilising the very latest air induction technologies.

The River Island Warehouse was fitted with multi storey mezzanines and, contrary to what many people believe, air distribution with these mezzanine areas differs significantly from a conventional Warehouse Heating & Cooling Solution. Many warehouse operators assume that air will find its own way into these mezzanine areas because they are fitted within a ventilated space; the reality is that this is not the case.

Challenges

The main issues that required careful consideration were overheating of occupants and lack of ventilation. The Industrial Warehouse was served by 4 No. AHUs, 2 No., externally serving the main warehouse and, 2 No. AHUs internally serving the high-level mezzanine areas. It was particularly critical to ensure that adequate ventilation was supplied into the body of the mezzanine and the appropriate amount of supply air was delivered to each level – providing a comfortable and productive working environment, and meeting health and safety requirements.

River Island case study River Island case study

Solution

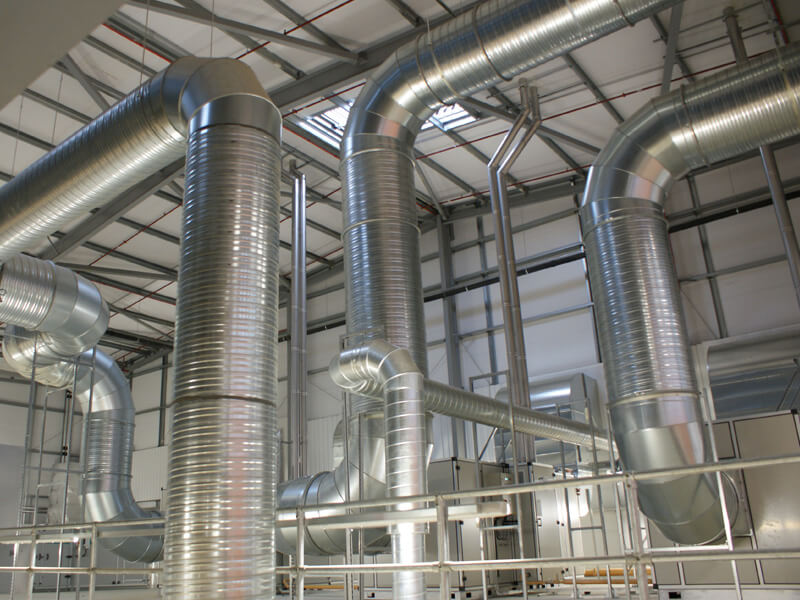
Our Industrial Heating & Cooling Systems are the ideal solution for creating the desired Climate Control throughout the mezzanine areas. The High Velocity System can provide Heating, Cooling and Ventilation into the body of the mezzanine, creating a comfortable and productive working environment. Small diameter unobtrusive ductwork is used to deliver the treated air into the body of mezzanine via a series of self-balancing air induction nozzles. The ductwork system is connected to a centralised AHU, which can be located either internally or externally.

Air Technology Systems are Industrial Climate Control Specialists, providing solutions including Extraction, Warehouse Heating, Cooling, Heat Recovery, Replacement Air Input and Odour Control. Working closely with clients, consultants and other engineering professionals, our design and project team offers a wealth of experience in the industry.

Read More – Climate Control

Biomass Ventilation System

Biomass Ventilation System

Biomass Ventilation System

Air Technology Systems worked with our client, in the Energy from Waste market, to manage their Industrial Ventilation issues at their new facility.

Client

A leading organisation in Engineering & Manufacturing for the Pharmaceutical & Medical Industry.

Project Scope & Objectives

We were discussing several challenges with our client that needed addressing on their new Biomass EfW facility and had already installed a Cyclone Dust Extraction System, to address the dust problems associated with handling wood chip biomass.

The decision had been made that the feedstock for the facility was going be changing from biomass (wood chip) to Refuse Derived Fuel (RDF). This presented other issues that needed to be considered because the new fuel type, derived from waste, could potentially be odorous.

Collaborating with the Client, we proposed a design for this issue, proceeding to supply, install, and commission the systems.

Challenges

  • Contain & treat the air within the Fuel Reception Building (FRB)
  • Reduce the potential for fugitive emissions to escape the FRB
  • Incorporate the requirements of the client’s gasification process

Solution

The simplest way of treating the odorous air from the FRB was to direct that air volume to the gasifiers that were part of the EfW facility.

We designed a ventilation system that would extract the air from the FRB and transfer it to the air intake for the gasifiers.

In addition to the extract system, we installed their innovative Industrial Ventilation supply system which contributed two key functions:

  • Minimise the potential for escape of odours – high velocity nozzles ware arranged above and around the vehicle doors to ‘push’ air toward the rear wall of the building.
  • Maximise the effective capture of the odours – the extraction ductwork is positioned on the rear wall of the building and works in conjunction with the Industrial Ventilation ‘pushed’ air volume, to ‘pull’ the air into the extract ductwork system.

The nature of the air within the FRB was unknown, however, since it could be aggressive, and that and the proximity of the site is only 5km from the coast (saline environment), we installed plastic ductwork which has excellent corrosion resistance:

  • Industrial Ventilation supply system – uPVC
  • Extract / transfer system – uPVC and uPVC/GRP wrapped

We provided full integration and communication of the various system control panels and instrumentation with the site BMS.

In addition to the above, the Client asked Air Technology Systems to liaise and organise the other aspects of work that were also recommended as part of the solution, these included:

  • Installation of fast acting doors on the FRB
  • Installation of a misting system within the FRB – both dust suppression & odour control systems
  • Installation of full height curtains to separate the building into clean (no dust) and dirty (dusty) areas
  • Various modifications to the original building to ensure that the new system would operate effectively.

Result

Air Technology Systems and our Client worked on a collaborative basis to develop the systems and ductwork designs that would result in effective solutions for the potential problems that can arise on an EfW site, ensuring that the Client would meet their planning requirements.

ATS Plastics Capabilities

The plastic ductwork for projects such as this can all be fabricated by ATS Plastics; we have full in-house capabilities with high specification manufacturing equipment to ensure we can fabricate big quantities of ductwork of any size efficiently and to a high-quality standard.

All plastic ductwork associated with this project ranged from 400dia to 1200dia including fittings such as bespoke transition pieces, non-return dampers, isolation dampers and actuated dampers. The external ductwork was GRP wrapped for 2 reasons:

  1. Structural integrity as the duct was 1200 dia
  2. Provide UV protection which can age and speed up the process of the ductwork becoming brittle from the temperature abuse of the UK weather.

With the ductwork being GRP, wrapped it meant the client could select the colour of the ductwork they wanted to fit either with their planning permission requirements or to fit in with the aesthetics of the site.

Read More – Plastic Ductwork Read More – Industrial Ventilation

Heating, Cooling & Ventilation System for new Sorting Hall

Climate & Ventilation System for Sorting Hall

A new Heating, Cooling and Ventilation System for the company’s new South Midlands sorting hall.

Client – Royal Mail

Project Scope & Objectives

To design and install a Heating, Cooling, and Ventilation System into the new sorting hall at Swan Valley, meeting the specific business requirements of the mail sorting warehouse and its staff, for a temperature-controlled environment.

Challenges

This project presented several challenges that we needed to overcome, including:

  • Maintaining a comfortable controlled temperature, for staff working in the sorting hall
  • Infiltration of outside temperatures, through large loading doors
  • Designing a solution that would provide low ongoing energy costs
  • Meeting the sustainability requirements of Royal Mail

Solution

Air Technology Systems designed and installed an air induction system using our high velocity nozzle technology with four air handling units (AHUs), two of which are connected to a solar wall.

The AHUs provide in excess of 1000kW of mechanical cooling and 600kW of heating with AHU 1 being supplied by a building biomass system, AHUs 2 & 3 being indirect gas-fired units connected to the solar wall and AHU 4 being an indirect gas-fired unit for discharging the exhaust gases.

The system is controlled via the Trend DDC Controller to maximize the renewable energy source during daylight hours.

Result

The sorting hall’s Heating, Cooling and Ventilation System at Swan Valley is saving Royal Mail 233,396 kW a year to deliver energy and cost savings.

The system also reduces CO² output by 59 tonnes a year, which helps meet the company’s sustainability and environmental requirements.

As the system is based on central plant arrangements and a self-balancing system, there is now no need for any high-level maintenance. Running costs are reduced by positioning the AHU’s close to the gas and electrical supplies, along with the added benefit of the solar wall.

The Industrial Heating, Cooling & Ventilation System can also be operated on full fresh air in summer to provide free cooling and ventilation, and further savings on running costs.

Read More – Climate Control

Odour Control and Lighting Wastewater Treatment Site

Odour Control Electrical Case Study

Odour Control and Lighting Wastewater Treatment Site

ATS Electrical were required to Design & CDM Project Manage the Installation of both a Form 4 Control Panel and the lighting for this Wastewater Project.

Client – Wastewater Treatment Site

Project Scope & Objectives

The design and installation of a Form 4 control panel and electrical installation to WIMES and specific water industry specifications. It needed to control a new odour control system, comprising of 2no. biological filter units, 1no. droplet eliminator, 2no. duty stand-by centrifugal exhaust fans with emergency stop, heat extraction, thermistors, flow switches and motor heaters, 3no. carbon filter units, 2no. pressure transmitters, motorised water supply valves, trace heating and panel heaters and flow and limit switches.

Additionally, Air Technology Systems took on the Construction Design Management (CDM) role for this project, completing the removal of redundant PLC code and HMI mimics relating to old plant and new SCADA signals to be integrated with existing site wide system.

Air Technology Systems were also awarded the design, supply and installation of emergency and task lighting to cover the extent of the new installation.

Challenges

Due to this site being a live site, with a fully working process area and the works involving the replacement of an old system, we needed to utilise and change some of the, already in-place, wiring ducts. This needed to be a fast-paced project delivery to reduce “downtime” of the old system, to reduce odours affecting nearby public areas.

It was essential for us to interface with the clients controls system and their external specialists, to adapt the existing feeders and SCADA system for utilisation and commissioning.

Whilst designing the project, we were also required to install a new Form 4 panel in the new Kiosk, due to increased size and capabilities.

We had to ensure WIMES and specific water industry specification to be met with the panel build and full electrical installation, while large amount of Interfacing with new mechanical odour control plant and existing infrastructure was essential to ensure a smooth all round project delivery.

Electrical Control diagram Odour Control Electrical Case Study

Solution

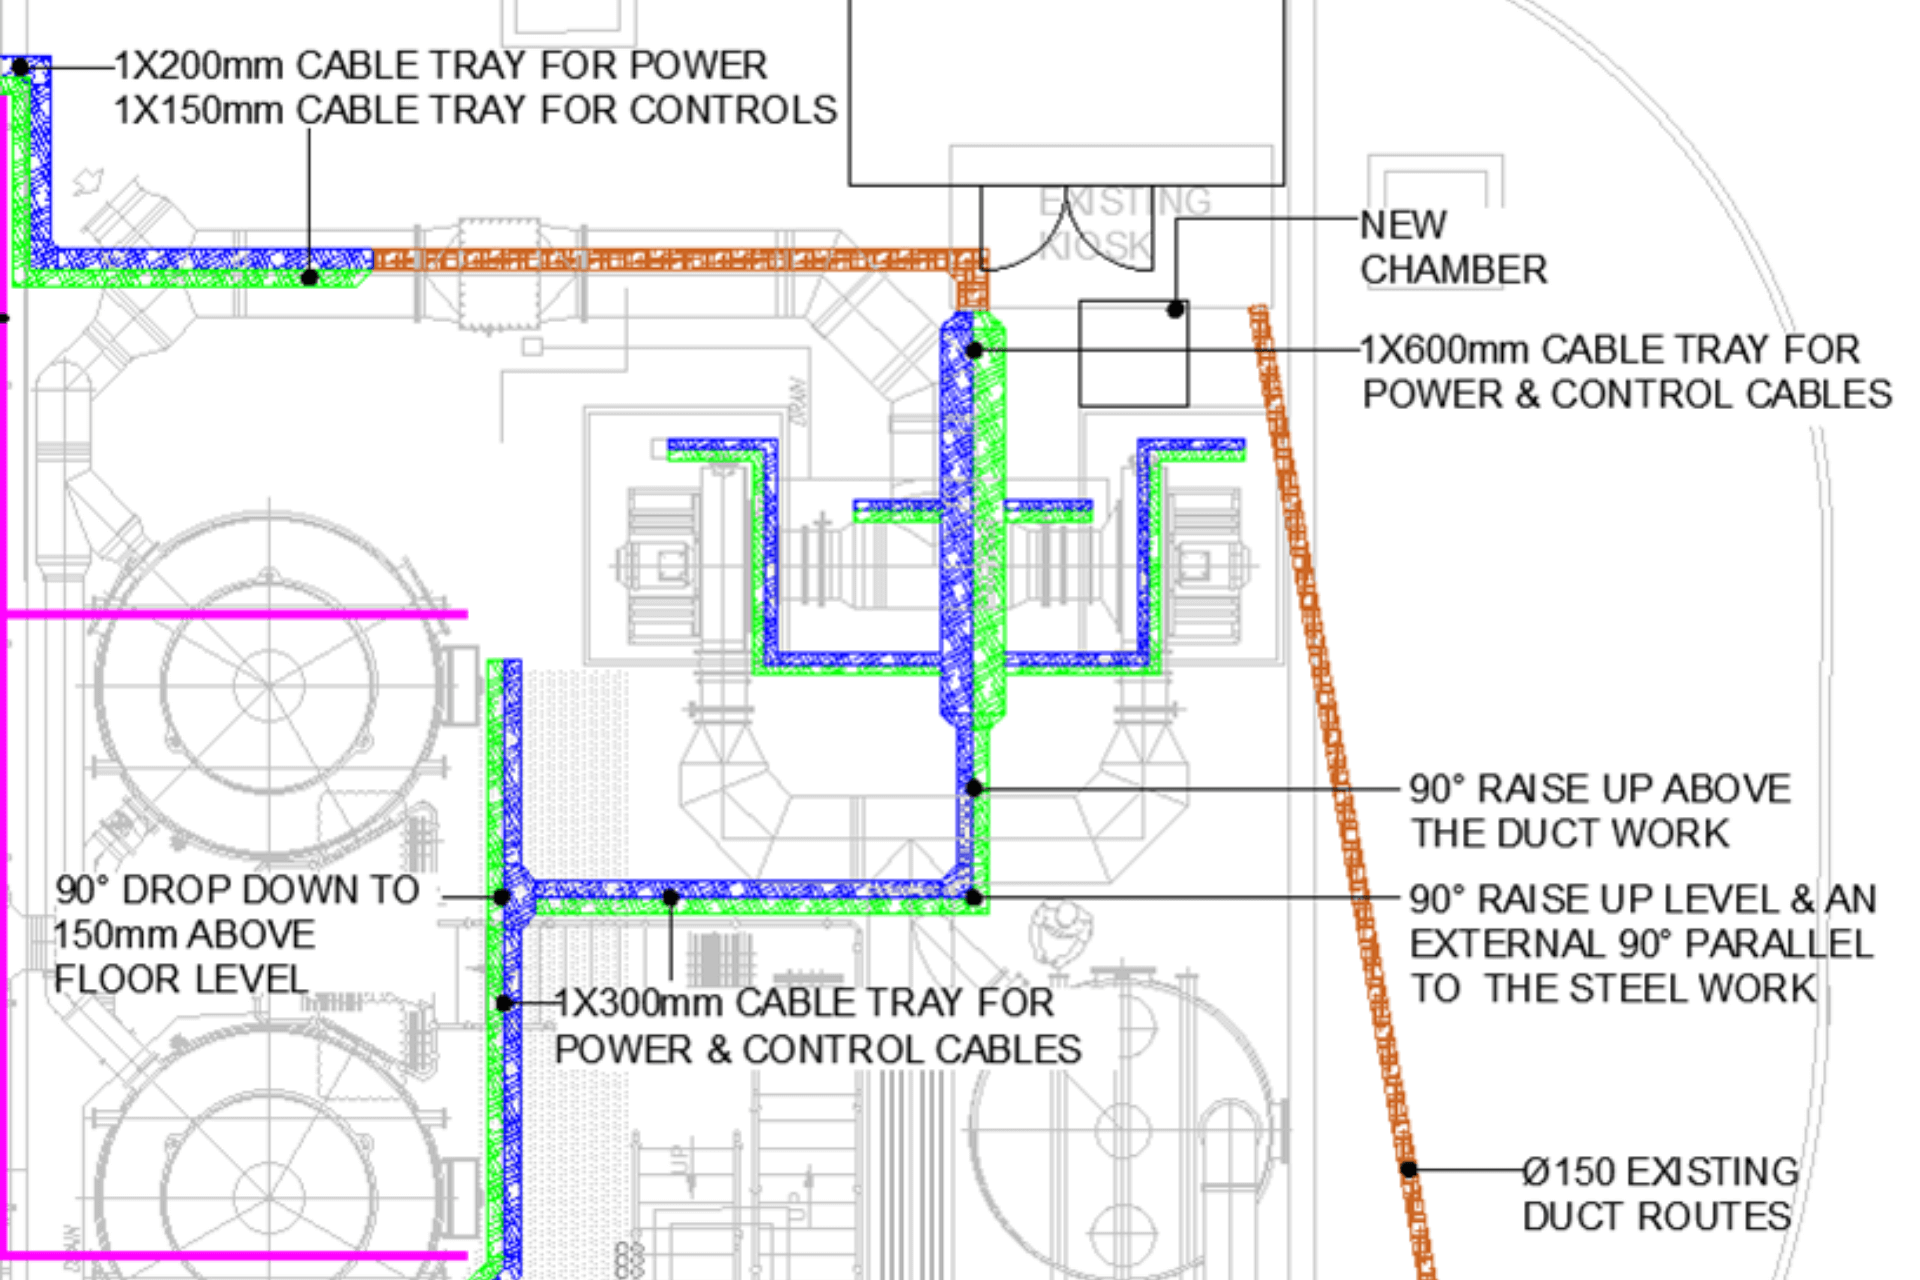
We created new wiring routes with the use of existing wiring ducts and above-ground, heavy duty, post-dipped galvanised tray work to serve all items of kit. This enabled a fast-paced project delivery, while we increased the size of our installation team to reduce overall programme duration.

Due to the complex nature of this project, we positioned on-site, non-working supervisors to assist with smooth CDM project management.

With the new size of Form 4 panel needed, we installed and positioned a new kiosk (4.5m x 2.5m) to house the controls and distribution. To meet with project deadlines, the kiosk was lifted into position after the installation of the control panel, with a temporary waterproof marquee installed to facilitate full installation.

We used our in-house labour team to carry out this project, who have a wealth of experience relating to WIMES and numerous water body specifications, along with our internal Electrical and Mechanical Design teams worked closely to ensure a seamless functional design was provided

Result

As a result of firm teamwork, value engineering and client support; we ensured a fully functional Odour Control and emergency lighting systems were designed, installed, and commissioned to high specification-compliant standards.

We guaranteed both internal and client collaborations, throughout the course of the project, resulting in programme deadlines being met in good time, without any changes to quality or philosophy.  At the end of this successful project, all new plant and controls were seamlessly integrated and commissioned alongside local site PLC/HMI and regional SCADA, the emergency lighting installation was installed to a high standard as per design calculations and layout; and tested without issue.