Specialist Ventilation Solution for the Lee Tunnel Project

Lee Tunnel Ventilation

Specialist Ventilation Solution for the Lee Tunnel Project

Air Technology Systems Limited are design and project management specialists with over thirty years of experience in providing effective, energy saving systems for industrial Climate Control & Odour Control Solutions.

Client – Thames Water

We are working with MVB for Thames Water on the Lee Tunnel Project, London: the largest, deepest vertical tunnel in Europe.

Project Scope & Objectives

Air Technology Systems are providing both a specialist Industrial Ventilation Solution, combined with innovative rope access installation methodology within the new Main Shaft Pumping Station at Beckton Sewage Treatment Works, as part of the prestigious and ground-breaking Lee Tunnel Project.

The Lee Tunnel is the first of two tunnels being constructed for Thames Water, which will collectively capture sewage from various combined sewer overflows (CSOs), built by the Victorians as part of an ageing sewerage network that still serves London 150 years on.

The four-mile tunnel will run beneath the London Borough of Newham from Abbey Mills to Beckton, and it will help prevent more than 16 million tonnes of sewage mixed with rainwater overflowing into the river Lee each year, by capturing it and transferring it to Beckton Sewage Treatment Works, which is being expanded to enable it to deal with the increased volumes of sewage and flood water.

A new main shaft pumping station is being constructed within a 38m diameter, 80m deep shaft at Beckton and linked to the main Lee Tunnel. The main area of the Pumping Station will be divided into two dry well compartments which shall house the pumps and motors to pump the storm water into Beckton STW for treatment.

In addition, the pumping station has two designated access shafts to allow safe ingress and egress from the pumping station for maintenance.

Air Technology Systems have worked in the water industry as specialist ventilation and odour control providers for 20 years and were approached by MVB to quote for the ventilation for this specialist project.

Solution

Design

Air Technology Systems were chosen to deliver the ventilation package because of our innovative design and installation methods. The ventilation systems to serve the main shaft are designed to achieve a safe working environment for operatives due to the risk of hydrogen sulphide being present, but additionally to overcome the huge heat gain from the large pumps.

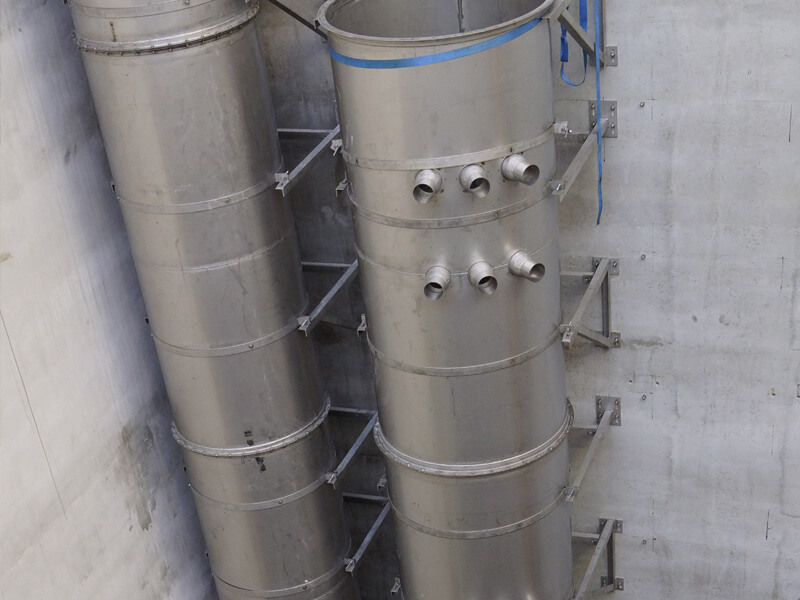
Air is supplied to both sides of the shaft via large plants located outside the shaft with large vertical ductwork being used to distribute air evenly throughout the drywells. We have further innovated using our original air induction nozzles which are key to achieving a high ventilation efficiency by thoroughly mixing the air, diluting any heat and contaminants such as hydrogen sulphide and creating the best possible working environment.

Air is extracted from low level from both sides of the shaft, another key design feature being that hydrogen sulphide is heavier than air and so collecting air at low level is another way we have increased the ventilation efficiency. Pumps are also located at low level and so we can capture heat at source and exhaust to outside.

The Access Shafts had different design requirements with a need to provide both general ventilation to the stairways, but also to pressurise the entire access shafts for firefighting. The system has been fully designed in accordance with BS EN 12101-6:2005 to provide a Class B system for means of escape and firefighting.

The design process has been challenging with lots of aspects to consider including selection of materials.

The entire main shaft ductwork system is 316 stainless steel sections to achieve a 20-year design life and with some of the ducts being 2.2m diameter we have used specialist construction techniques. Due to the depth of the pumping station replacement of ductwork will be very difficult and so selection of the correct materials is important.

The entire access shaft ductwork systems are 316 stainless steel sections, but fire rated for 4 hours.

Installation

Probably the biggest challenge on this project was how we would safely complete the installation. Conventional methods such as scaffolding and man riders were considered, but it was impossible to use this method because of the space available and of course would have a larger environmental impact using two cranes.

Installation via rope access was devised as the ideal solution as it allows access to install pipework, electrics, and ventilation systems within areas where scaffolding would traditionally be required, but would be inappropriate, prohibitively expensive, or unsafe.

At about the same time as this, an A/C system was being fitted on the 9th floor, in a light-well of a building that had multiple owners/landlords. The time taken to receive the necessary permissions to erect scaffold would have meant costly delays to the project.

Both challenges were overcome with a new innovative solution: the combination of IRATA rope access methods with the technical trade skills our operatives already had. Combining two existing skills is a major innovation in construction that has led to ATS being able to solve problems and provide solutions on both small and very large scales.

The Air Technology Systems rope access team is the only one in the World that can install the huge ventilation system on The Lee Tunnel Project, in the required location.
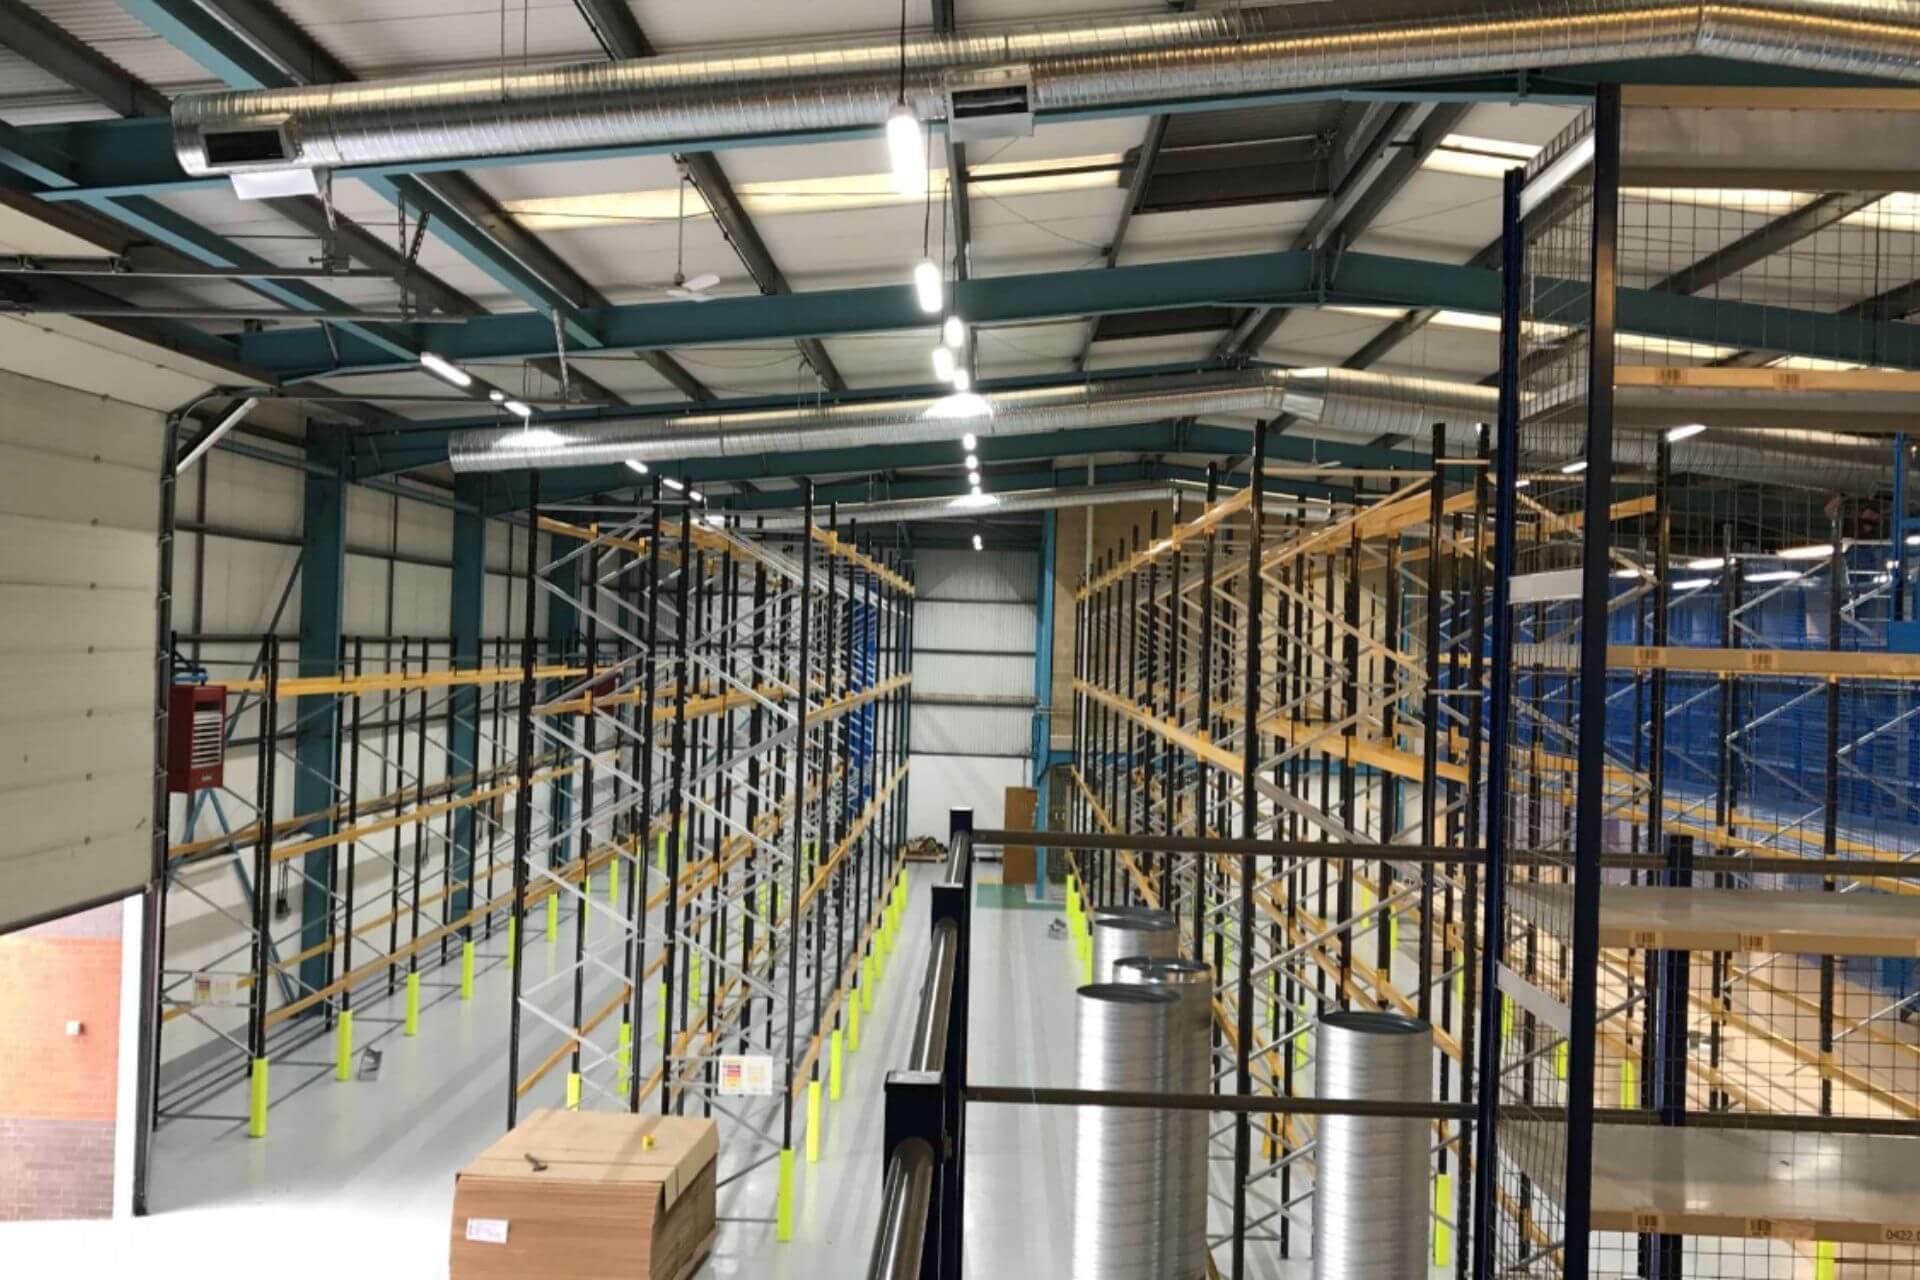
Pharmaceutical Warehouse Cooling Solutions for a Storage Facility

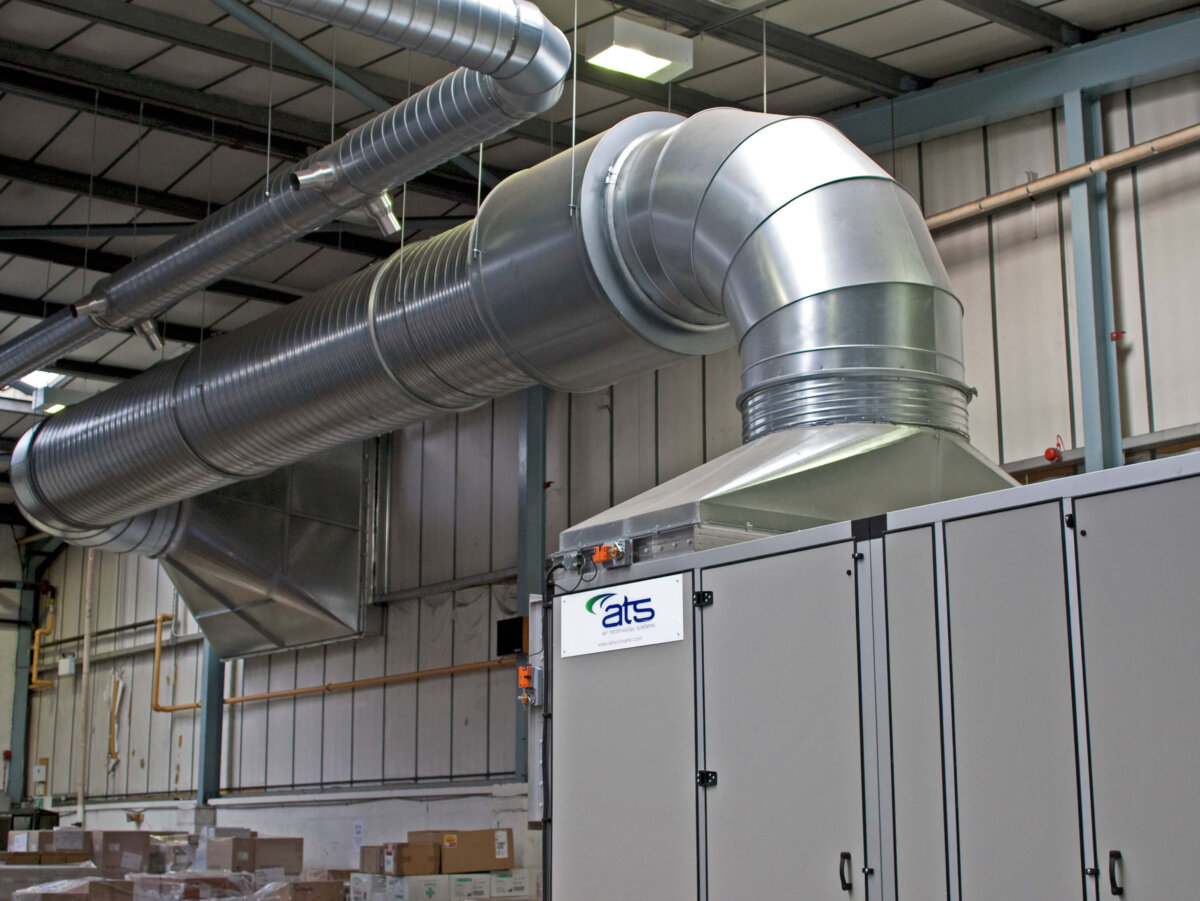
Warehouse Industrial Climate Control System AHU Ductwork

Pharmaceutical Warehouse Cooling Solutions for a Storage Facility

We needed to provide a Warehouse Climate Control Solution, to comply with stringent pharmaceutical guidelines.

Client – Pharmaceutical

A leading independent PLC based in the South East is one of the largest pharmacy chains in the UK and Europe.  As well as a strong pharmacy base, the Group contains a central distribution division with its warehouses supplying over 4,000 pharmaceutical products to its 300+ retail pharmacies across southern England.

Project Scope & Objectives

To provide a temperature-controlled solution (15-25°C) into the Croydon warehouse facility to meet the MHRA’s regulations, and manufactures stringent product specification. In addition, the system needed future proofing to take into account changing MHRA regulations and higher summer time temperatures.

Not meeting the requirements of the MHRA regulations can mean:

  • The suspension of a company’s wholesale distribution licence
  • Compulsory variation of licences to exclude certain activities
  • Sanctions and legal action against the Responsible Person
  • Loss of a company’s distribution licence altogether

Challenges

Air Technology Systems had several challenges to consider and overcome with this project, some of which were:

  • Even temperature distribution to ±1°C
  • Unevenly populated areas, including packed mezzanine areas
  • The need for high energy-efficiency and low running costs
  • A tight deadline
  • Installing within an operational working environment

Solution

To achieve all the project’s goals, Air Technology Systems installed an air induction heating, cooling & ventilation system.

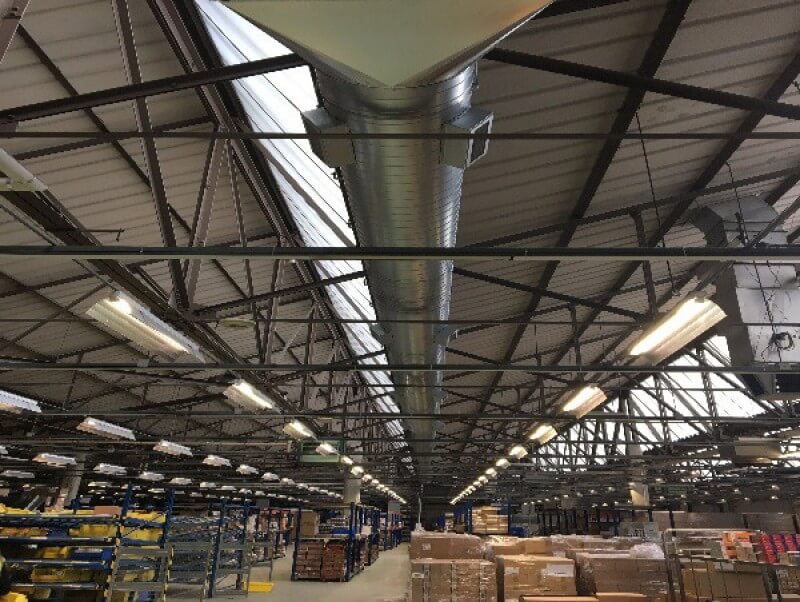
Main ducting at roof level, as well as unobtrusive small diameter ductwork with self-balancing nozzles, provided even horizontal and vertical total temperature control throughout the warehouse.

The ductwork system was connected to a centralised Air Handling Unit (AHU) at ground level, outside the building. And to further ease and speed up the installation time, the AHU was supplied on a skid to enable it to be slotted straight into position.

To compliment the Industrial Climate Control System, Yanmar Gas Heat Pumps can work in conjunction to provide a highly efficient air conditioning solution. Clients can then benefit from further reductions in both running costs, typically 40%, and electrical power requirements, typically 90% reduction, when compared to conventional air conditioning systems.

Result

Our specialist-designed Air Handling Units enable night-purge ventilation, which gives free summer cooling to significantly lower energy costs and reduce the company’s carbon output.

The company’s designated Responsible Person now have complete peace of mind that their Croydon warehouse facility is storing the company’s pharmaceuticals within the temperature band stipulated by the MHRA regulations at all times.

Visit Yanmar Website

Odour Control at Newbury Sewage Treatments Works

Odour Control System

Odour Control at Newbury Sewage Treatments Works

Air Technology Systems needed to replace existing Odour Control Units that were in place at Newbury Sewage Treatment Works.

Client – Thames Water

Project Scope & Objectives

Thames Water had two non-functional Odour Control Units (OCU’s) on site that needed to be removed and replaced:

  1. Bio-scrubber OCU which treated the Picket Fence Thickener (PFT) Area
  2. Acid Scrubber OCU which treated the Centrifuge Area

Air Technology Systems were employed to decommission and remove these OCU’s and identify, design and provide a replacement Odour Control Solution.

Challenges

  • Treating odours from numerous sludge storage and treatment processes across the site.
  • Uncertainty about whether the processes of liming sludge was going to remain on site – Important as this would determine the type of abatement selected.
  • Odour loads and concentrations had changed from original installation. New basis of design was provided by Thames Water.
  • Underground extract ductwork that needed ‘capping off’ and re-routing above ground.
  • The largest volume of air to be treated came from the skip room and the capture of odours in this area needed to be improved.
  • Thames Water needed a company that was prepared to take on the role of Principle Designer and Contractor and deliver the project complying with CDM regulations 2015 and responsibilities.
  • A full Mechanical, Electrical, Instrumentation, Control and Automation (MEICA) package with the addition of Civil and Structural works were to be incorporated into the contract.
  • Some assets were in a poor state of repair – the requirement for repair / replacement of the tank lids on both the ‘raw sludge PFT’ and ‘raw sludge buffer’ tanks were identified during one of the pre-start site visits.

Prior to the award of a contract Air Technology Systems proactively engaged with Thames Water and together worked collaboratively to determine the solution that would best meet all of their requirements.

Solution

Air Technology Systems recommended that the two existing OCU’s were replaced with a single multi-stage OCU.

The decision was made that there would be no further ‘liming’ taking place on site, and therefore there was no risk of ammonia odours. This in turn meant that the incorporation of an acid scrubbing stage was not a requirement

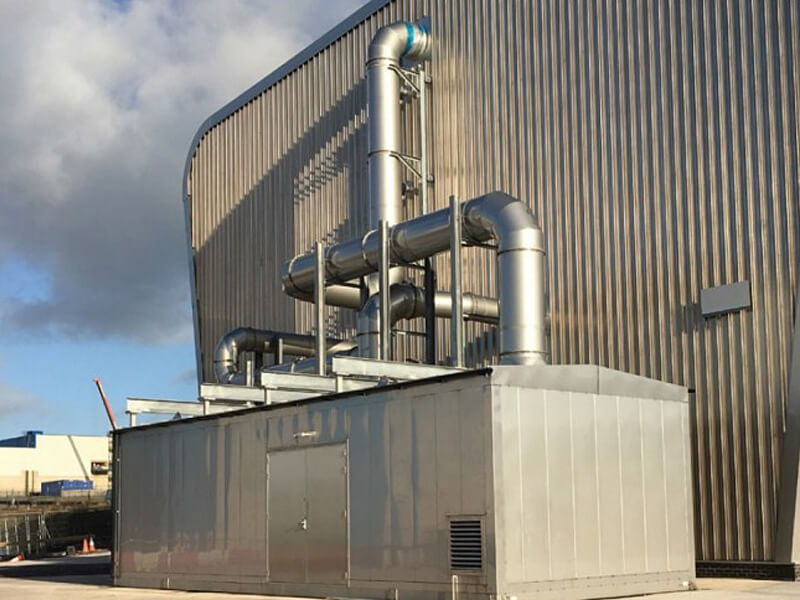
Both existing OCU’s were dismantled and removed from site, to be replaced by the new, two stage OCU consisting of:

  • Stage 1: 2 x bio-trickling filters treating and removing large volumes of hydrogen sulphide (H2S), mercaptans and other sulphur-based compounds associated with Wastewater and Sludge Treatment.
  • Stage 2: 3 x carbon filters to ‘polish’ any remaining odorous compounds and achieve an odour discharge level of <1000OuE/m3 or 50ppb H2S

To ensure efficient treatment of the odours, and minimise the size of the odour control vessels, we used an innovative solution so that only sources of odour classed as ‘high odours’ were treated in the bio-trickling filters and then the carbon filters. The ‘lower odour’ air (which was the largest volume of air) bypassed the bio-filters and was only treated by the carbon filters.

This resulted in an efficient treatment of odour and a lower overall capital and operating cost as the existing OCU footprint was maintained.

ATS replaced or modified much of the existing extract ductwork. Two duct bridges were installed to carry the ductwork across roadways on the site, 1 bridge spanned 16m.

In addition to extract duct modification in the skip room, Air Technology Systems installed their high-velocity nozzle supply system. This Industrial Climate Control System is designed to maximise the ventilation efficiency, it was utilised on this project to ensure increase mixing of air & dilution within the skip room and improving the efficiency of the extract system.

Air Technology Systems also installed a dedicated Form 4 MCC panel to provide automation of the Odour Control System. This was housed in purpose-built GRP Kiosk.


Result

Through the process of collaborative development, the Odour Control Solution designed, supplied, installed, and commissioned by Air Technology Systems was the optimum system to combat the odour challenge.

The solution was fully compliant with all applicable Thames Water Asset Standards and importantly, because Air Technology Systems were communicating directly and effectively with the end user – Thames Water – we were able to introduce & discuss innovative aspects to the solution that were accepted on their merits as well as increasing the speed and efficiency of project delivery.

Henry Crompton, Project Manager for Thames Water commented:

“From initial engagement with ATS, it was apparent that they had a refreshing approach to this project and introduced some clever and constructive ideas. They have taken the role of CDM co-ordinator within their stride and delivered a very professional and most importantly safe installation. Overall, I’m very happy with ATS and hope I get the opportunity to work with them again”

Warehouse Cooling Solutions for United Drug Sangers, Belfast

Pharmaceutical Warehouse Cooling

Warehouse Cooling Solutions for United Drug Sangers, Belfast

Air Technology Systems provided Industrial Modular Cooling & Heating Solution for a 7,500m2 Pharmaceutical Warehouse.

Client – United Drug Sangers

When supply chain services company United Drug Sangers had concerns with the operation and functionality of the existing cooling system in their distribution warehouse, they called upon us to provide a new cooling solution that would meet its sustainability requirements and specific business needs, whilst using the very latest air induction technology.

Project Scope & Objectives

We needed to provide a Climate Control System, specifically our high velocity Modular Cooling system, to comply with the strict MHRA guidelines. This project had to be undertaken in an operational building due to time constraints, including night-time working.

The benefits of using an ATS high-velocity system approach are:

  • Full design responsibility for system performance
  • We have completed many previous installations within Pharmaceutical Warehouses
  • Familiar with the requirements of the MHRA
  • We can include out of hours working
  • Full site supervision during the installation period
  • Modular Cooling for ease of installation
  • Low operational costs due to high ratio mixing system combined with effective control systems.
  • The system met the client’s requirements for improved climate control, lower operational cost, and low maintenance needs.

Challenges

To overcome the issue of working around operational hours, we had discussions with the client and agreed times suitable to allow us to be on site and complete the installation outside of normal working hours.

The modular version of our Industrial Climate Control System was selected as there was insufficient space to install a centralised plant. Large ductwork is thus unnecessary and also limited the amount of time working over track and machinery. The modular approach to this project enabled zonal heating and cool thereby further reducing operational costs.

Solution

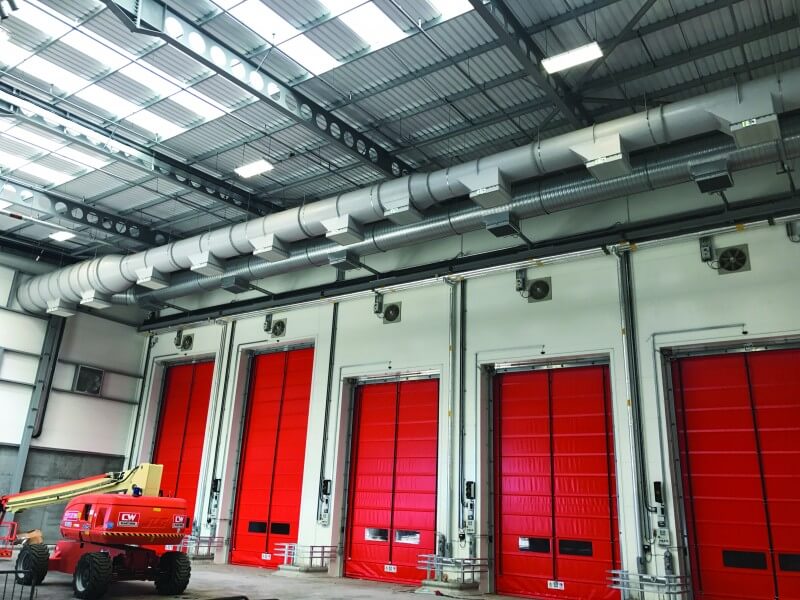
The Industrial Climate Control System provided was designed to control the treated warehouse areas to comply with MHRA temperature requirements. By using the Modular Cooling system, the air is distributed throughout the space via a series of high-velocity distribution ductwork systems and balanced air distribution nozzles.

The air induction nozzles produce an air induction ratio of up to 15:1 providing high mixing of the air thus preventing micro-climates within the space and giving even horizontal and vertical temperature gradients. It is critical that a high-velocity type approach is used in this application to efficiently deal with the high bay warehouse areas and reduce temperature variations.

Result

To complete this project to the agreed schedule, we made a detailed plan with the client for installation areas and times. A progress plan of operations was not only issued to the client but placed on the local information boards for all operatives to be aware of.

Areas and times were agreed and cordoned off and the installation commenced speedily due to the safe practices and aid of the client and the site team. Due to the co-ordination of the project the client did not lose any working time and fulfilled all their daily orders and the project was completed earlier than the planned programme.

Industrial Ventilation System for a New Waste Treatment Centre

Industrial Ventilation Waste Treatment Centre

Industrial Ventilation System for a New Waste Treatment Centre

Air Technology Systems won the project for a New Waste Treatment Centre located in Derby, in which they were required to provide an Industrial Ventilation System.

Client – Interserve

Interserve, who in partnership with Shanks Waste Management (now Renewi), formed Resource Recovery Solutions (RRS) Derbyshire to manage waste for Derby City Council and Derbyshire County Council.

Project Scope & Objectives

To supply and install ventilation solutions within the new facility, which included several different areas with varying challenges, including:

  • Reception Bays and Hall
  • Oversize Area
  • MRF Hall
  • RDF Bunker
  • ACT Hall & Basement
  • FGT Hall
  • Turbine Hall
  • Ash Bunker

Challenges

Before Air Technology Systems joined the project, a ventilation scheme had been designed by a consultant, to support the planning application. This meant we had to work within the significant restrictions of that accepted design.

Further challenges included:

  • The initial scheme design using air extraction only to achieve the required outcomes
  • Constraints on the total air volume that could pass through a pre-designed biofilter
  • No allowance being made for vehicle emissions within the reception bay area

Solution

We used a variety of forced air techniques, including our proprietary high-velocity nozzle system, to ensure effective air movement in critical areas.

Air Technology Systems designed a separate system, complete with odour control, to provide the additional air change requirement for the reception bay area due to the vehicle emissions.

Throughout the project Air Technology Systems continued to recommend improvements as required and demonstrated excellent Project Management skills on a site that had numerous contractors all trying to complete their part of the scheme!

Ventilation System for a New Building at Sellafield

Nuclear Ventilation

Ventilation System for a New Building at Sellafield

Air Technology Systems were to design and install a complete, highly efficient, Ventilation System for a new building at Sellafield.

Client – Morgan Sindall

Long-term client, Morgan Sindall is part of the Infrastructure Strategic Alliance (ISA), which has a £1.1 billion contract to deliver a range of infrastructure asset services to the Sellafield site.

Project Scope & Objectives

  • To check and validate the outline design.
  • To supply and install an Industrial Ventilation System to provide Climate Control within the new building.

The system needed to maintain:

  • A winter minimum of 15°C at -4°C (heating)
  • A summer maximum of 20°C at 24°C (cooling)

Challenges

This was our first major nuclear project; therefore it presented a number of challenges:

  • Significantly higher technical specification and quality levels across the entire project
  • The security requirements that needed to be fulfilled and the physical logistics of working within a highly protected and secure nuclear decommissioning site
  • Understanding the culture of Sellafield and this very sensitive industry
  • In addition to the industry-related challenges, we had the physical challenge of Sellafield’s coastal location and the associated aggressive and corrosive environment

Solution

From first discussions, we liaised with Morgan Sindall for a full understanding of all the implications associated with working on the Sellafield site.

Our innovative decision to manufacture, assemble and test all equipment off-site saved project time and money and enabled full inspection prior to delivery. In total, 75% of commissioning was completed off-site.

To combat the corrosive nature of the coastal location, all external equipment was constructed from high grade stainless steel with a 60-year lifetime.

Result

Air Technology Systems helped to exceed all the project’s goals with completion achieved in a quicker time frame than predicted and with the overall project an impressive £11M under budget.

This outcome was reflected in Morgan Sindall’s project assessment, where the company scored ATS a ‘good to excellent’ 9/10 in nine categories and an ‘excellent’ 10/10 in four categories, namely, Innovation, Technical Support, Management and Delighted Customer. All of which gave us an overall assessment score of 92%. The project also received a ‘Sellafield Award for Return on Investment’.

Ventilation and Odour Control System for Andigestion

Odour Control Unit

Ventilation and Odour Control System for Andigestion

This new-build Anaerobic Digestion Facility required a high-efficiency, Industrial Ventilation & Odour Control Solution.

Client – Andigestion Ltd

Andigestion Ltd designs and operates commercial scale anaerobic digestion plants for processing industrial and domestic food waste to create renewable energy and nutrient-rich fertilizer.

Project Scope & Objectives

As part of Andigestion’s bid to deliver a new Anaerobic Digestion facility for Gloucestershire County Council, Air Technology Systems were asked to:

  • Design an odour control system for the waste reception building, based on Environment Agency (EA) guidelines of 3 air changes per hour (ac/hr)
  • Provide best value whilst maximizing effectiveness

Challenges

To adopt the E.A. guidelines of providing a ventilation/extraction rate of 3 air changes per hour was going to be prohibitive, due to the size of the odour control footprint, and the capital costs associated.

Air Technology Systems therefore needed to work collaboratively with the client to find a way to effectively capture and treat the odours generated from the food waste Anaerobic Digestion facility.

The Odour Control System also needed to be capable of treating a wide range of undefined odour compounds often associated with food waste Anaerobic Digestion facilities.

Solution

The design of the solution involved:

  • Where possible, capture of odours as close as possible to their source
  • Installation of our Industrial Ventilation System to significantly increase the efficiency of the ventilation within the building
  • Installation of curtains to contain odour within areas where we could capture it more effectively
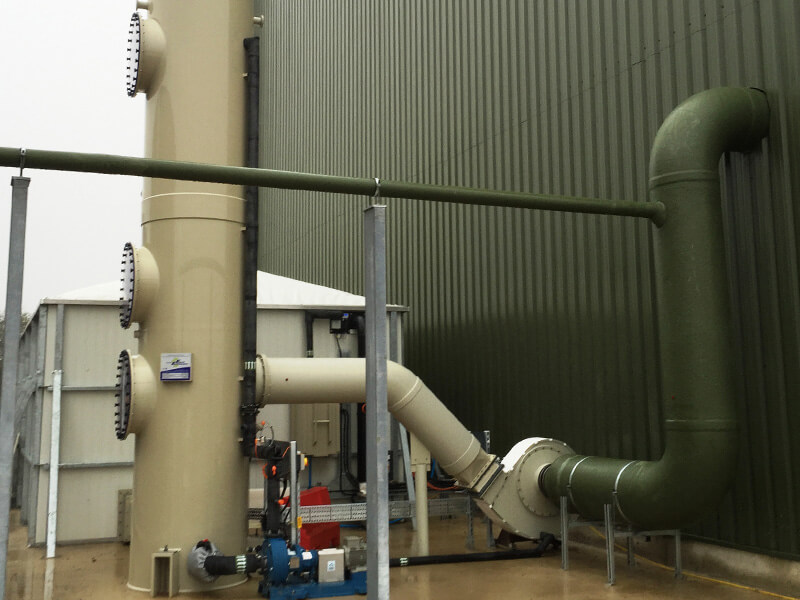
  • Odour Control System comprising of a water scrubber and organic biofilter

The E.A. were kept informed of our approach, and in particular the fact that we were not going to provide 3 ac/hr for the whole building

Result

  • Size of OCU significantly reduced
  • Operating costs reduced due to smaller fans and media quantity etc
  • Effectively ventilated building and no odour complaints
  • Acceptance of design by Environment Agency
  • Happy customer

Temperature Control Systems for AAH Warehouses

AHU Ductwork

Temperature Control Systems for AAH Warehouses

The Design & Installation of Temperature Control Systems for multiple existing and operational Pharmaceutical Warehouses.

Client – AAH

The largest pharmaceutical wholesaler in the UK. From 16 distribution warehouses, the company delivers around 15 million products to more than 14,000 pharmacies and other organisations every week.

Project Scope & Objectives

To design and install a Warehouse Heating, Cooling and Ventilation System for all AAH’s distribution warehouses. The system had to provide uniform temperature control across a variety of different paces, in order to meet the strict requirements (low/high temperature range 15°C -25°C) of the MHRA and the pharmaceutical manufacturers.

Not meeting the requirements of the MHRA regulations can mean:

  • The suspension of a company’s wholesale distribution licence
  • Compulsory variation of licences to exclude certain activities
  • Sanctions and legal action against the Responsible Person
  • Loss of a company’s distribution licence altogether

Challenges

  • All the warehouses were existing and fully operational buildings
  • Installation needed to be completed without disruption to operations
  • Some of the older buildings had a low source of electrical site power
  • The variety of spaces gave a wide range of ambient temperatures from cold spots around loading bays to excessive solar heat gains on mezzanines
AHU Ductwork Pharmaceutical warehouse cooling

Solution

To achieve all project goals, Air Technology Systems designed and installed Industrial Air Induction Heating, Cooling & Ventilation Systems in all the Pharmaceutical Warehouses.

The systems comprised of: Gas Heat Pumps; Air Handling Units (AHUs); high distribution ductwork; air induction nozzles and integrated controls packages.

Result

The Industrial Climate Control System’s design enabled air from the hot spots to be circulated to cold spots, saving mechanical heating costs.

The Gas Heat Pumps solved the issue of low site electrical capacity, and with a co-efficient of performance between 115% and 135%, they will also supplement winter heating. The Gas Heat Pumps (GHPs) will reduce AAH’s gas usage, and in turn their running costs and carbon footprint.

Choosing Air Handling Units from the Government’s Carbon Trust Energy Technology List enabled AAH to claim the Enhanced Capital Allowance. This meant lower capital costs and ongoing savings on energy costs and a further reduction of the company’s carbon footprint.

AAH now has peace of mind that all of its warehouse facilities store pharmaceuticals to MHRA regulations and manufacturer guidelines.

Climate Control for Food Distribution Warehouse

Food Storage Warehouse Ventilation

Climate Control for Food Distribution Warehouse

ATS provided a temperature-controlled frost protection system for a food distribution warehouse based in Ipswich.

Client – LDH (LA Doria) Ltd

One of the world’s largest, family-owned own label supplier of canned and dried goods to the leading UK supermarket chains.

Project Scope & Objectives

Our client required us to design, supply and install a fully temperature-controlled frost protection system, for their newly acquired food distribution warehouse in Ipswich, which included a 40m high bay area. The required temperature to be achieved throughout the warehouse for protection of the sprinkler system was 5°C.

The warehouse itself was divided into 3 main sections: the low bay, the 40m high bay and the mezzanine. The high bay alone had an area of 8280m², which meant we were working at heights throughout the industrial temperature control project.

Challenges

The biggest challenge faced by the team was due to the sheer height of the high bay area alongside the tight deadline and relatively short time frame given: 6 weeks. This meant work on the project needed to be fast-paced throughout and included careful coordination with other trades to ensure the project was completed to a high quality, in-line with the client specification and on time.

At over 40m high, the biggest requirement of the frost protection system was to ensure a constant and even temperature distribution, both horizontally and vertically, throughout the high bay area. A large percentage of the works had to be carried out at the 40m roof-level height, therefore specialist equipment was required on site to gain full access. This was not a problem for ATS, as all our staff who are required to work at heights are IPAF (International Power Access Federation), PASMA (Prefabricated Access Suppliers Manufacturers Association), and harness trained; this is a basic requirement to operate any MEWP (Mechanical Elevating Work Platform) on site.

ATS, having been in the industry for over 30 years, had the right temperature control expertise, knowledge, and training to be able to take on a unique and challenging project such as this one.

Food Storage Warehouse Ventilation

Solution

As our Temperature Control specialist sales team took the time to gain an in-depth knowledge and understanding of what the client required, it meant that our dedicated team designed an air induction system utilising our warehouse heating technology with 3 specialist air handling units (AHU’s).

To achieve an even temperature distribution throughout the areas, especially the 40m high bay area, the design team had to meticulously select ductwork routes, sizes and the appropriate equipment in order to meet the temperature requirements.

A total of 750KW of heating was supplied to the warehouse and over 1000m of ductwork was installed within the short time frame given. One ahu was dedicated to heating the mezzanine area, another AHU was dedicated to serve one side of the high and low bay areas, and the third AHU was dedicated to serve the other half of the high and low bay areas, resulting in even warehouse temperature distribution.

Result

The hard work and dedication given by the onsite project management team meant the warehouse heating goals were met within the project deadline and to the high exacting standard that ATS continuously provide.

Our warehouse heating system maintained a constant air temperature of 5°C, providing frost protection, throughout the high bay and low bay areas, as well as heating the mezzanine area.
Our specialist temperature control engineers worked around the clock to provide our client with a successfully installed, high specification warehouse heating system, designed for one of the UK’s largest high bay areas.

The project was completed within the time frame and within budget, and the best result of all was a happy client.

Read More – Climate Control